Why Thread Gauges Are Often Under-Budgeted
New production lines are usually budgeted around machines, tooling and fixtures. Thread gauges appear late, often as a single line such as “inspection equipment”, and the number is guessed from the last project. When the line starts, operators share one gauge set between three machines, final inspection borrows from the toolroom, and the first worn GO plug stops production while a replacement is made.
A thread gauge budget does not have to be complicated. It needs a thread list, a clear view of where each thread is checked, a rule for spares and a line for calibration. With those four elements, the budget can be built in an afternoon and defended in a project review.
Step 1: Build the Thread List
Go through every part drawing that will run on the new line and list each distinct thread. Record the full designation, including pitch and class, and note whether the thread is internal or external. Two parts with the same thread share the same gauge type, so the list is of thread specifications, not of part features.
| Thread | Internal / external | Parts using it | Condition when gauged |
|---|---|---|---|
| M6x1-6H | Internal | Housing, cover | Finished |
| M10x1.5-6H | Internal | Housing | Finished |
| M10x1.5-6g | External | Stud | Before plating |
| 1/4-20 UNC-2B | Internal | Export bracket | Finished |
| G 1/4 | Internal | Housing port | Finished |
| 1/2-14 NPT | Internal | Valve port | Finished |
Include the gauging condition. A thread checked before plating and the same thread checked after plating may need two different gauges. Our guide to gauging before or after plating explains when this applies.
Step 2: Count the Inspection Points
Every place where a thread is checked needs its own gauge, unless gauges genuinely move with the parts. Sharing gauges between stations saves money on paper but costs time and invites mix-ups in practice.
| Inspection point | What it does | Typical gauge need |
|---|---|---|
| At the machine | First-off, tool change and periodic checks | One working set per machine or cell running the thread |
| Final inspection | Sampling or 100% check before shipment | One working set per final inspection station |
| Incoming inspection | Checks bought-in threaded parts | One set per purchased thread specification |
| Quality lab or reference | Referee checks and disputes | One set kept as reference, used rarely |
| Toolroom | Tap and tool set-up | Optional, often shared with the machine set |
Multiply the number of threads by the number of points at which each is checked. That gives the number of working GO/NO-GO sets. For example, a thread cut on two machines and checked at final inspection needs three working sets, plus a reference set if your quality plan uses one.
For guidance on machine-side checking frequency, see how GO/NO-GO thread gauges are used.
Step 3: Plan Spares for Wear
GO members wear faster than NO-GO members because they run the full length of every good thread. NO-GO members engage only briefly, within the two-turn limit under ISO 1502 or the three-turn limit under ASME B1.2. So spares should be planned mainly as GO members, not complete sets.
Materials also matter. Abrasive materials such as cast iron and some aluminium alloys, and threads with burrs or chips, wear gauges faster. The thread plug gauge wear limits article explains how wear is judged at calibration.
A spare that is not calibrated is not a spare. Spare gauges should be received, registered and calibrated like working gauges, then stored ready for use. A spare that has never been checked cannot be put into service in a hurry without a quality risk.
Step 4: Ring Gauges and Setting Plugs
External threads add a decision about setting plugs. Unified inch ring gauges are commonly adjustable and set with setting plugs under ASME B1.2 practice. Solid metric ring gauges made to ISO 1502 can be verified by a calibration lab without setting plugs, although some plants still buy them.
If you calibrate ring gauges in-house, budget one set of setting plugs per ring size and class, not per ring. Setting plugs are used only in calibration, so one set can serve several working rings of the same specification. Read do thread ring gauges need setting plugs? before deciding.
Step 5: Build the Budget by Cost Category
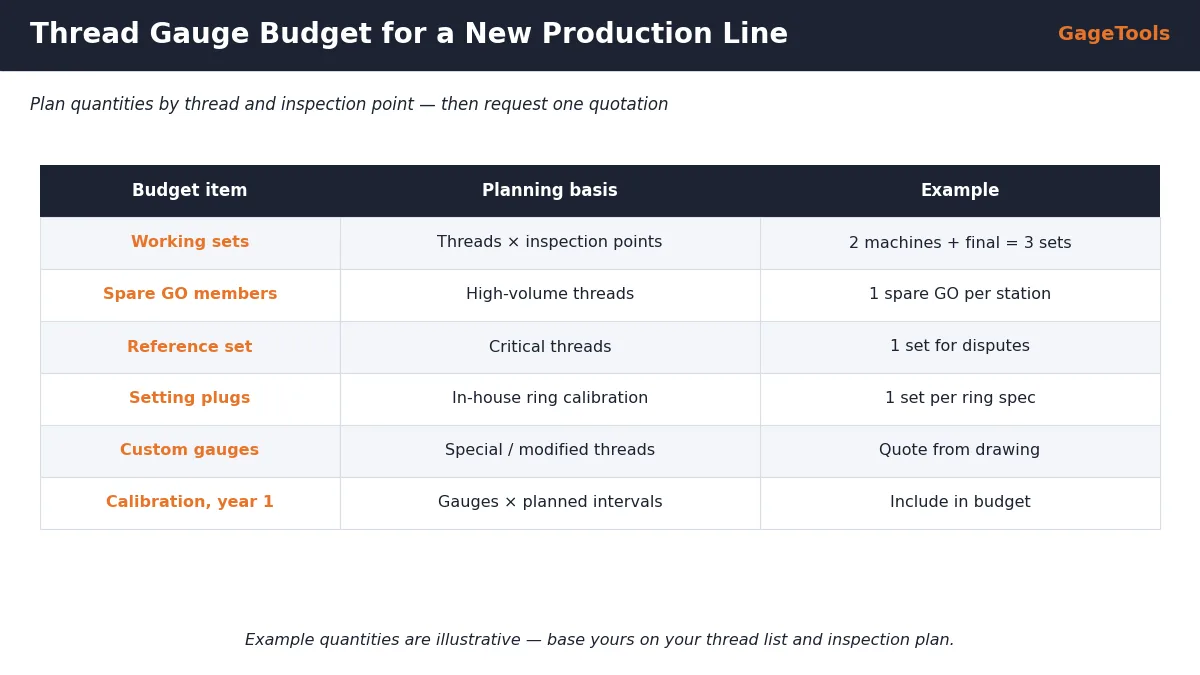
Gauge prices vary with size, thread system, class and whether the gauge is standard or custom, so it is better to build the budget by category and then request a quotation for the complete list. Our thread gauge price guide explains what affects each price.
| Budget category | What it covers | How to estimate |
|---|---|---|
| Working gauge sets | GO/NO-GO sets for each inspection point | Threads × inspection points |
| Spare GO members | Replacement for high-wear threads | Per high-volume thread and station |
| Reference sets | Referee and dispute checks | One per critical thread |
| Setting plugs | In-house ring calibration | One set per ring specification |
| Custom gauges | Special threads, modified limits, special handles | From drawing-based quotation |
| Calibration, year one | Periodic calibration of all gauges | Number of gauges × planned intervals |
| Storage and handling | Cases, racks, labels | Per station |
Keep the budget linked to the thread list. When a part changes, the gauge quantities update with it, and nobody has to rebuild the numbers from scratch.
Step 6: Match Gauge Delivery to the Project Plan
Gauges should arrive before the first trial parts, not with them. Operators need gauges for tool set-up and first-off approval, and the quality team needs time to register and calibrate them. Standard sizes ship from stock within 72 hours; custom gauges made to drawings take 10–15 working days, plus shipping.
- Freeze the thread list when the part drawings are released for tooling.
- Issue the gauge order at the same time as the cutting tool order.
- Approve custom gauge drawings quickly so manufacturing can start.
- Register and calibrate gauges on arrival.
- Issue gauges to stations before trial production begins.
If the line has many special threads, plan the custom gauges first; they set the critical path. Drawing-based gauges also need a short review of the gauge design before manufacturing starts, so allow a few days for questions and approval on top of the manufacturing time.
Plan the ramp-up as well. Gauge usage is usually highest during trial runs and early production, when set-ups are repeated and parts are checked more often. That is when wear on GO members is fastest, so having the spares on the shelf from day one avoids an early stoppage.
Common Budgeting Mistakes
| Mistake | Consequence | Better practice |
|---|---|---|
| One gauge set shared across the line | Queues and mix-ups at machines | One set per inspection point |
| No spare GO members | Line stops when a GO plug wears out | Spares for high-volume threads |
| Forgetting plating condition | Wrong gauge for coated threads | Record condition on the thread list |
| No calibration budget | Gauges go out of date | Include year-one calibration |
| Ordering gauges after tooling | Trial parts cannot be approved | Order gauges with cutting tools |
What to Send When Ordering Gauges for a New Line
For a quotation that matches your budget structure, send:
- The thread list with full designations, classes and hand
- Quantity of working sets per thread and number of spare GO members
- Gauging condition for each thread (before or after plating)
- Whether setting plugs and reference sets are required
- Drawings for any special or modified threads
- Required delivery date for first trial parts
- Certificate requirement per line (ISO/IEC 17025 available on request)
We can quote the complete list on one purchase order. See our thread plug gauges and thread ring gauges pages for standard ranges.
Planning Thread Gauges for a New Production Line?
Send your thread list, inspection points and delivery date. We propose quantities, flag special gauges early and quote the full list within 24 hours.
Related: Bulk thread gauges for OEM buyers · Thread gauge price guide · MOQ and lead time guide
Frequently Asked Questions
✓ 20+ years gauge manufacturing
✓ ISO 9001:2015 certified
✓ In-house CNC grinding & inspection
✓ Drawing / RFQ reply within 24h
Thread Gauges for Your New Production Line
GageTools supplies complete thread gauge packages for new lines: GO/NO-GO plug and ring gauges, spare GO members, setting plugs and custom gauges from drawings. ISO/IEC 17025 calibration certificate available on request. Standard sizes ship from stock within 72 hours; custom gauges in 10–15 working days. MOQ 1 piece. WhatsApp for fastest response.
💬 WhatsApp Quote 📐 Send Drawing for Quote