// Direct Answer
A GO/NO-GO thread gauge is a pass/fail inspection tool used to verify that a threaded part — bolt, nut, or tapped hole — is within its specified tolerance. The GO gauge must pass fully under hand pressure; the NO-GO gauge must not engage more than two turns. A part passes only when both conditions are true simultaneously. GO/NO-GO gauges are available as plug gauges (internal threads) and ring gauges (external threads), covering all major thread standards including Metric, UN, BSP, and NPT.
Quick answer: A GO/NO-GO thread gauge checks whether a thread is inside its tolerance zone without measuring it. The GO member must assemble by hand over the full thread length (the thread is not too tight); the NO-GO member must not assemble beyond a few turns — typically no more than two turns under ISO 1502 and three under ASME B1.2 (the thread is not too loose). A part is accepted only when both checks pass.
The GO/NO-GO Principle — Taylor’s Principle of Gauging
GO/NO-GO gauging is based on Taylor’s Principle, which states that the GO gauge should check as many thread elements as possible simultaneously — pitch diameter, major diameter, minor diameter, pitch, and thread angle — while the NO-GO gauge should check only one element at a time, specifically the pitch diameter at the maximum material condition.
This two-member system gives a complete functional verification of the thread in a single inspection cycle, without requiring any dimensional measurement. The result is binary — pass or fail — making it fast, reliable, and independent of operator interpretation.
GO GAUGE — FULL FORM
The GO gauge is a full-form gauge — it has the complete thread profile. It checks all thread elements simultaneously. It verifies that the thread is not too tight to assemble.
Must pass freely under hand pressure only → Part passes GO test
NO-GO GAUGE — SINGLE ELEMENT
The NO-GO gauge checks only the pitch diameter at the maximum material condition. It verifies that the thread is not too loose — has not been machined beyond the upper limit.
Must stop within 2 turns under hand pressure → Part passes NO-GO test
Two-turn rule: The NO-GO gauge is allowed to engage up to but not more than two full turns. This allowance accounts for the thread lead-in chamfer at the start of the workpiece thread, which may have a slightly different form. If the NO-GO engages more than two turns, the pitch diameter is beyond the maximum material limit — the part is rejected.
Need GO/NO-GO gauges for this thread?
GageTools manufactures GO/NO-GO thread plug gauges from USD 20 and thread ring gauges from USD 30. MOQ 1 piece, stock sizes ship within 72 hours, and a calibration report or ISO 17025 certificate is available on request.
Thread Plug GaugesThread Ring GaugesRequest a QuoteTypes of GO/NO-GO Thread Gauges
🔌 GO/NO-GO Thread Plug Gauge
For internal threads · Nuts · Tapped holes
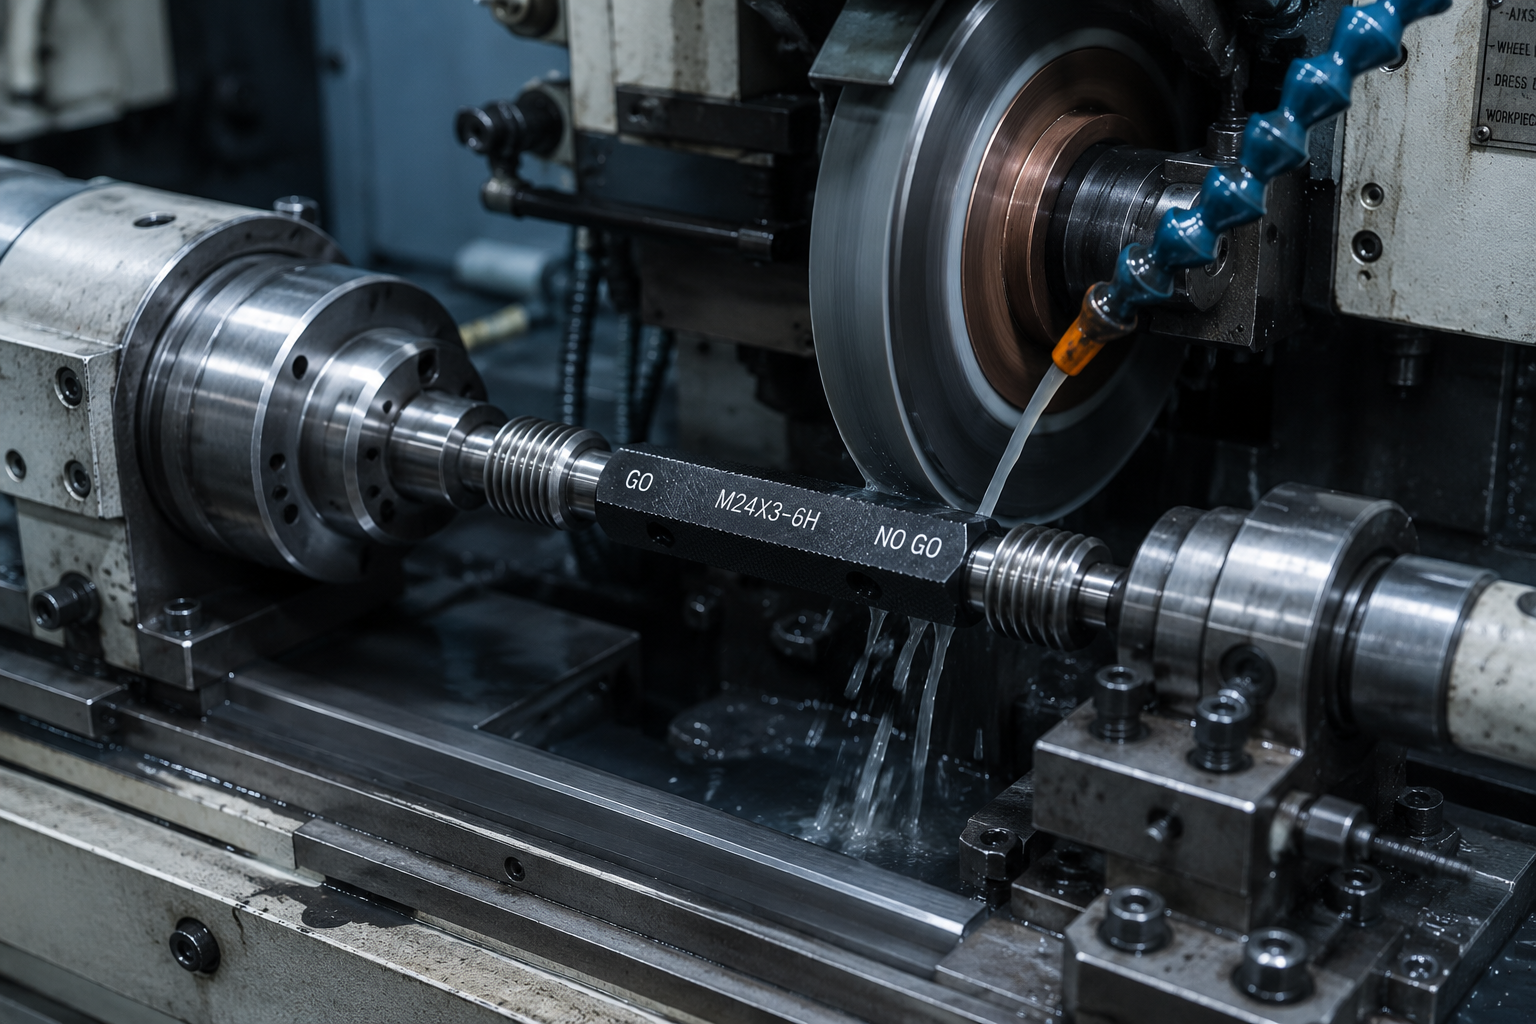
Inserted into the internal thread. The GO end must thread through the full hole length. The NO-GO end must not engage more than two turns. Usually double-ended on one handle — GO on one end, NO-GO on the other.
Tolerance classes: 4H · 5H · 6H · 7H (metric) · 1B · 2B · 3B (UN)
→ Full Thread Plug Gauge Guide
⭕ GO/NO-GO Thread Ring Gauge
For external threads · Bolts · Studs · Shafts
Placed over the external thread. The GO ring must thread over the full bolt length. The NO-GO ring must not engage more than two turns. Always supplied as two separate rings — GO and NO-GO are not double-ended.
Tolerance classes: 6g · 6e · 4g · 6h (metric) · 1A · 2A · 3A (UN)
→ Full Thread Ring Gauge Guide
| Property | GO/NO-GO Plug Gauge | GO/NO-GO Ring Gauge |
|---|
| Inspects | Internal (female) threads | External (male) threads |
| Typical parts | Nuts, tapped holes, inserts, pipe ports | Bolts, studs, shafts, pipe fittings |
| GO/NO-GO format | Double-ended on one handle (small sizes) | Two separate rings always |
| Inspection action | Inserted into the hole | Placed over the part |
| Default metric tolerance | 6H | 6g |
| Standard | ISO 1502 / ASME B1.2 | ISO 1502 / ASME B1.2 |
Need GO/NO-GO gauges? Send your thread callout.
Plug & Ring · Metric · UN · BSP · NPT · ISO/IEC 17025 cert · 72hr delivery · MOQ 1
Reading GO/NO-GO Inspection Results
The GO/NO-GO system produces four possible result combinations. Only one of them is a pass. Understanding each combination helps diagnose what is wrong with a rejected part.
GO Gauge
NO-GO Gauge
Decision
Likely Cause
✓ Passes fully
✓ Stops ≤ 2 turns
ACCEPT
Thread is within tolerance — assemble
✗ Does not pass
Any result
REJECT
Thread oversize, damaged flanks, wrong pitch, or tap broken in hole
✓ Passes fully
✗ Passes > 2 turns
REJECT
Thread undersize (too loose) — pitch diameter below minimum material limit
✗ Does not pass
✗ Passes > 2 turns
REJECT
Severe thread damage — inspect visually before scrapping
Never force a gauge to get a different result. If the GO gauge does not pass freely, the part fails — forcing the gauge through will damage the gauge thread and produce false results on subsequent inspections. The correct action is to reject the part and investigate the machining process.
GO/NO-GO Inspection Procedure — Step by Step
1
Verify gauge calibration status
Check the calibration label on the gauge or its case. Confirm the calibration date is within the valid interval (typically 6–12 months). If the gauge is overdue for calibration, remove it from service before proceeding. See our
Thread Gauge Calibration Guide for calibration intervals.
2
Clean the workpiece thread and the gauge
Wipe both the thread being inspected and the gauge with a clean lint-free cloth. Remove chips, cutting fluid, and debris. For fine pitch threads, use a soft brass brush in the thread roots. Never inspect a contaminated thread — chips between gauge and workpiece cause false rejections and accelerate gauge wear.
3
Apply light instrument oil (fine pitch threads)
For threads with pitch below 1.0mm (metric) or above 20 TPI (UN), apply a thin film of instrument oil to the gauge thread. This reduces friction without affecting the measurement result. Do not use grease or heavy oil — these trap particles and cause false rejections.
4
Apply GO gauge — hand pressure only
For plug gauges: insert GO end into the tapped hole and rotate by hand. For ring gauges: place GO ring over the bolt and rotate by hand. The GO gauge must pass through or over the full thread length under hand pressure only. If it passes freely — GO test passed. If it does not pass — part rejected.
5
Apply NO-GO gauge — hand pressure only
For plug gauges: insert NO-GO end. For ring gauges: place NO-GO ring. The NO-GO gauge must NOT engage more than two full turns under hand pressure. If it stops within two turns — NO-GO test passed. If it enters more than two turns — part rejected. Never force the NO-GO gauge.
6
Record and decide
GO passes AND NO-GO stops within two turns = Accept. Any other combination = Reject. Record the result with gauge serial number, calibration date, operator ID, and part/batch reference. This is required for ISO 9001 clause 7.1.5 traceability. Store the gauge in its case immediately after use.
GO/NO-GO Gauge Standards by Thread Type
| Thread Standard | Gauge Standard | Default Tolerance — Internal | Default Tolerance — External |
|---|
| Metric ISO (M series) | ISO 1502 | 6H (plug gauge) | 6g (ring gauge) |
| UN — UNC / UNF / UNEF | ASME B1.2 | 2B (plug gauge) | 2A (ring gauge) |
| BSPP (G thread) | ISO 228-2 | G (plug gauge) | G A / G B (ring gauge) |
| BSPT (R / Rc thread) | ISO 7-2 | Rc (taper plug) | R (taper ring) |
| NPT | ANSI B2.1 | L1 taper plug | L1 taper ring |
| ACME | ASME B1.5 | 2G / 3G (plug) | 2G / 3G (ring) |
For a full size chart and dimensional data for each standard, see our Thread Charts reference page covering Metric, UN, BSP, and NPT thread dimensions.
How to Select the Right GO/NO-GO Gauge
Selecting a GO/NO-GO gauge requires four pieces of information from the engineering drawing. Missing any one of them results in an incorrect gauge being ordered. For a complete selection guide, see Thread Plug Gauge vs Ring Gauge: How to Choose.
| Information Needed | Example |
|---|
| Thread standard & size | M12 · 1/2-13 UNC · G 1/2 |
| Pitch / TPI | ×1.75 · 13 TPI |
| Tolerance class | 6H · 6g · 2B · 2A |
| Internal or external | Plug gauge · Ring gauge |
QUICK RULE
Thread inside a part → Plug Gauge
Thread outside a part → Ring Gauge
No tolerance shown (metric) → 6H / 6g
No tolerance shown (UN) → 2B / 2A
For a detailed explanation of all tolerance classes — 4H, 5H, 6H, 7H, 6g, 6e, 4g — see Thread Gauge Tolerance Classes Explained. For calibration requirements and intervals, see Thread Gauge Calibration Guide. For storage and handling best practices, see Thread Gauge Storage and Handling.
Not sure which GO/NO-GO gauge to order?
Send your thread callout and drawing — we confirm gauge type, tolerance class and lead time in 24 hours.
Why a Part Fails GO/NO-GO Thread Inspection
When a thread is rejected, the gauge result points to the likely cause. Use this table to troubleshoot before you scrap parts or change tools.
| Result | Likely cause | What to check |
|---|
| GO plug will not enter the internal thread | Pitch or minor diameter too small, burrs or chips, damaged first thread | Clean and deburr, check tap size and tap wear, check the thread start |
| NO-GO plug enters past the allowed turns | Pitch diameter oversize, worn or oversize tap, tap run-out | Check the tap, spindle alignment and cutting conditions; re-check with a verified gauge |
| GO ring will not pass over the external thread | Pitch diameter oversize, damaged or deformed threads, plating thicker than allowed | Check pre-plate size allowance, thread rolling or die setting, handling damage |
| NO-GO ring passes the external thread | Pitch diameter undersize, worn die or rolls | Check die or roll wear and machine setting |
| Two gauges give different results | One gauge is worn or out of calibration, temperature difference | Verify both gauges against their calibration records and check the ring with its setting plug |
Gauge Wear, Calibration and Setting Plugs
GO members engage the full thread on every check, so they wear faster than NO-GO members. A worn GO plug becomes smaller and can start accepting internal threads that are actually too tight, so wear has to be controlled.
- Calibration interval: set by your quality system according to how often each gauge is used. High-volume GO members usually need checking more often than NO-GO members.
- Setting plugs (check plugs): thread ring gauges are adjusted and verified with a matching setting plug, so order the setting plug together with the ring gauge when your customer requires it.
- Traceability: keep a calibration certificate for each gauge serial number and retire the gauge when it reaches its wear limit.
- Handling: clean gauges before use, never force them, and store them oiled in their case to prevent rust and damage.
GO/NO-GO Gauges vs Variable Thread Measurement
GO/NO-GO gauges give a fast pass/fail answer. When you need actual values, for example for SPC or process capability studies, use a variable method alongside them.
| Method | What you get | Best for |
|---|
| GO/NO-GO thread plug or ring gauge | Pass / fail (attribute) | Production and incoming inspection, fast operator checks |
| Three-wire method | Measured pitch diameter of external threads | Gauge-room checks, disputes, verifying critical parts |
| Thread micrometer | Measured pitch diameter | Shop-floor measurement of external threads |
| Indicating thread gauge | Variable reading of pitch diameter | SPC data collection on high-volume threads |
Frequently Asked Questions
What is the difference between GO and NO-GO gauges?
The GO gauge verifies that the thread is not too tight to assemble — it checks all thread elements simultaneously and must pass through or over the full thread length. The NO-GO gauge verifies that the thread is not too loose — it checks only the pitch diameter at the maximum material condition and must stop within two turns. Both are required for a complete inspection: a thread can pass the GO test and still fail the NO-GO test if it has been machined too large (internal) or too small (external).
Can I use just the GO gauge without the NO-GO gauge?
Using only the GO gauge provides an incomplete inspection. The GO gauge confirms the thread can assemble, but cannot detect threads that are too loose — machined beyond the maximum material limit. In production inspection under ISO 9001, IATF 16949, or AS9100, a complete GO + NO-GO inspection is required. GO-only inspection is only acceptable in very specific, documented cases where the NO-GO condition is impossible by the nature of the process — and this exception must be justified in the control plan.
What does it mean when the NO-GO gauge passes?
When the NO-GO gauge passes — engages more than two turns — the thread pitch diameter is beyond the maximum material limit. For an internal thread (tapped hole), this means the thread has been cut too large and the mating bolt may have insufficient engagement. For an external thread (bolt), this means the thread is too small and the mating nut may be loose. In both cases the part is rejected. The most common causes are worn cutting tools, incorrect tap size, or incorrect machining parameters.
What is Taylor’s Principle and why does it matter for thread gauging?
Taylor’s Principle states that the GO gauge should simulate the mating part as closely as possible — checking all relevant dimensions simultaneously — while the NO-GO gauge should check only one dimension at a time. For thread gauging, the GO gauge has the full thread form (pitch diameter, major diameter, minor diameter, pitch, and angle all checked together), while the NO-GO gauge checks only the pitch diameter. This ensures that the GO test confirms functional assembly and the NO-GO test confirms dimensional conformance to the maximum material condition.
How do I know which GO/NO-GO gauge to order for my thread?
You need four pieces of information from the engineering drawing: thread standard and nominal size, pitch (metric) or TPI (UN), tolerance class, and whether the thread is internal or external. Internal threads (tapped holes, nuts) need a thread plug gauge. External threads (bolts, shafts) need a thread ring gauge. If no tolerance class is shown on the drawing, use 6H for internal metric threads or 2B for internal UN threads. See our full
Plug vs Ring Gauge selection guide for more detail.
Can GO/NO-GO gauges be supplied with a calibration certificate?
Yes. All GageTools GO/NO-GO thread gauges — plug and ring, metric and UN, BSP and NPT — can be supplied with an ISO/IEC 17025 calibration certificate on request. The certificate shows actual measured values for pitch diameter, major diameter, minor diameter, pitch, and thread angle. NIST-traceable. Accepted by ISO 9001, IATF 16949, and AS9100 auditors. For more on what the certificate contains, see our
Calibration Certificate Reading Guide.
How many turns can a NO-GO thread gauge enter?
A NO-GO thread gauge may start into the thread but must not go further than the allowed number of turns. Under ISO 1502 practice this is typically no more than two turns; under ASME B1.2 the NOT GO gauge must not exceed three complete turns. Always follow the standard and the drawing your customer specifies.
How often should GO/NO-GO thread gauges be calibrated?
There is no single fixed interval. Your quality system sets it based on usage: gauges used many times per shift, especially GO members, should be checked more often than gauges used occasionally. Record each check on the gauge calibration record.
Why do GO and NO-GO ends have different colours or markings?
Many gauges mark the GO and NO-GO members differently, for example with coloured bands or handles and engraved GO / NO-GO text, so operators cannot confuse the two ends during inspection.
Order GO/NO-GO Thread Gauges
Plug and ring gauges for Metric, UN, BSP, NPT, ACME. All tolerance classes. ISO/IEC 17025 calibration certificate available on request. MOQ 1 piece. Standard sizes ship in 72 hours.
✓ 20+ years gauge manufacturing
✓ ISO 9001:2015 certified
✓ In-house CNC grinding & inspection
✓ Drawing / RFQ reply within 24h
Click the email button to copy the address · Response within 24 hours
Pingback: Thread Plug Gauge vs Ring Gauge: Which One Do You Need?