The single most common ordering mistake for thread gauges is choosing the wrong type — a plug gauge when you need a ring gauge, or vice versa. This guide explains the difference in plain language, with a quick-selection table, inspection procedure, and everything you need to send an accurate RFQ.
Need gauges for this? GageTools manufactures GO/NO-GO thread plug gauges and thread ring gauges in Dongguan, China. Standard sizes ship from stock within 72 hours, MOQ is 1 piece, and every RFQ gets a reply within 24 hours — request a quote.
The Core Difference — One Sentence
Thread plug gauges inspect internal threads (nuts, tapped holes). Thread ring gauges inspect external threads (bolts, studs, shafts). That is the entire selection decision for 90% of applications.
Quick rule: Look at the part you are inspecting. If the thread is on the inside of the part — order a plug gauge. If the thread is on the outside of the part — order a ring gauge. If you are not sure, send a photo or drawing to WhatsApp +86 173 1689 5054 and we will confirm.
Thread Plug Gauge — Complete Guide
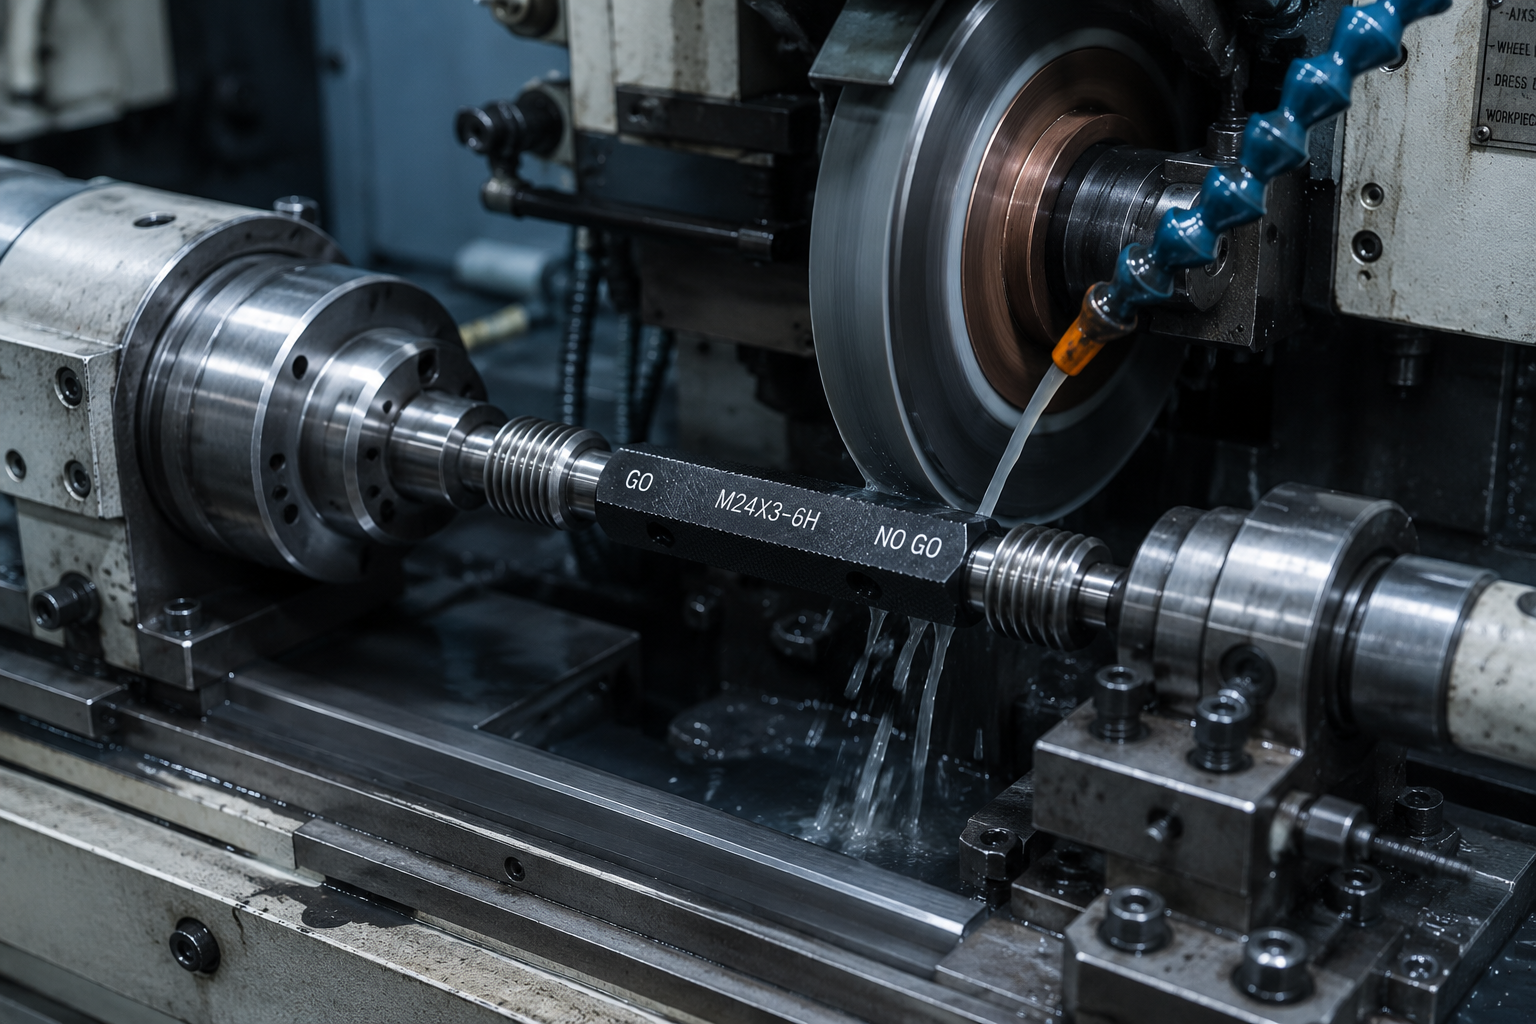
A thread plug gauge is a precision hardened steel plug manufactured to the exact GO and NO-GO pitch diameter limits of the specified thread standard and tolerance class. It is inserted into an internal thread to verify that the thread will correctly accept its mating bolt or stud.
Construction
Most thread plug gauges are double-ended — the GO gauge is on one end (usually marked with a green band or longer end) and the NO-GO gauge is on the other (red band or shorter end). The handle is colour-coded or engraved with the thread designation and tolerance class.
For larger diameters (typically above M100 or 4 inches), GO and NO-GO may be supplied as separate handles.
Where Thread Plug Gauges Are Used
| Application | Thread Type | Typical Tolerance |
|---|---|---|
| Nuts and hex nuts | Metric / UN / BSP | 6H / 2B |
| Tapped holes in machined parts | Metric / UN | 6H / 4H / 2B / 3B |
| Threaded inserts (Helicoil) | Metric STI | 6H STI |
| Pipe fittings (internal) | BSP / NPT / BSPT | G / Rc / NPT L1 |
| Engine blocks and housings | Metric / UN | 6H / 2B / 3B |
| Hydraulic and pneumatic ports | BSP / NPT | G / NPT |
Thread Ring Gauge — Complete Guide
A thread ring gauge is a precision hardened steel ring with an internal thread ground to the GO or NO-GO pitch diameter limits of the specified thread standard and tolerance class. It is placed over an external thread to verify that the thread will correctly enter its mating nut or threaded hole.
Solid vs Adjustable Ring Gauges
Solid ring gauges are the most accurate — the thread is ground to a fixed dimension and cannot be adjusted. They are recommended for production inspection and quality-critical applications.
Adjustable ring gauges can be reset using a setting plug gauge. They are used where the gauge needs to be recalibrated frequently, or where budget is a concern. Accuracy is lower than solid gauges.
Important: GO and NO-GO ring gauges are always supplied as two separate rings — unlike plug gauges which are usually double-ended. When ordering, always specify whether you need the GO ring, the NO-GO ring, or both as a set.
Where Thread Ring Gauges Are Used
| Application | Thread Type | Typical Tolerance |
|---|---|---|
| Bolts and hex bolts | Metric / UN | 6g / 2A |
| Studs and threaded rods | Metric / UN | 6g / 6e / 2A |
| Threaded shafts and spindles | Metric | 6g / 4g |
| Pipe fittings (external) | BSP / NPT / BSPT | G A/B / R / NPT L1 |
| Lead screws (ACME) | ACME | 2G / 3G |
| Automotive and aerospace fasteners | Metric / UN | 6g / 3A |
Full Side-by-Side Comparison
| Property | Thread Plug Gauge | Thread Ring Gauge |
|---|---|---|
| Thread location | Internal (female) | External (male) |
| Typical parts | Nuts, tapped holes, inserts | Bolts, studs, shafts |
| GO/NO-GO format | Usually double-ended (one handle) | Always two separate rings |
| Inspection action | Inserted into the hole | Placed over the part |
| Tolerance class (metric) | 4H / 6H / 7H (uppercase) | 6g / 6e / 4g (lowercase) |
| Tolerance class (UN) | 1B / 2B / 3B | 1A / 2A / 3A |
| Solid or adjustable | Solid only | Solid or adjustable |
| Standard | ISO 1502 / ASME B1.2 | ISO 1502 / ASME B1.2 |
| Wear pattern | GO end wears faster | GO ring wears faster |
| Calibration cert | ISO/IEC 17025 available | ISO/IEC 17025 available |
How to Choose — 4 Questions
Answer these four questions from your engineering drawing. You will have the correct gauge specification in under one minute.
Quick Selection Table
| What you are inspecting | Drawing callout example | Order this |
|---|---|---|
| Tapped hole in steel plate | M12×1.75-6H | M12×1.75 6H Thread Plug Gauge |
| Hex nut | M20×2.5-6H | M20×2.5 6H Thread Plug Gauge |
| Hex bolt | M12×1.75-6g | M12×1.75 6g Thread Ring Gauge |
| Threaded shaft | M30×3.5-6g | M30×3.5 6g Thread Ring Gauge |
| UNC tapped hole | 1/2-13 UNC 2B | 1/2-13 UNC 2B Thread Plug Gauge |
| UNC bolt | 1/2-13 UNC 2A | 1/2-13 UNC 2A Thread Ring Gauge |
| BSP internal port | G 1/2 (internal) | G 1/2 BSPP Thread Plug Gauge |
| BSP external fitting | G 1/2 A (external) | G 1/2 A BSPP Thread Ring Gauge |
| NPT internal pipe | 1/2-14 NPT (internal) | NPT 1/2-14 L1 Taper Plug Gauge |
| NPT external pipe end | 1/2-14 NPT (external) | NPT 1/2-14 L1 Taper Ring Gauge |
GO/NO-GO Inspection Procedure
The procedure is the same for both plug gauges and ring gauges. The only difference is the direction — plug gauges are inserted into the hole; ring gauges are placed over the part.
- GO gauge threads through fully under hand pressure only
- NO-GO gauge does NOT enter more than 2 full turns
- Both conditions must be true simultaneously
- GO gauge does not pass — thread is too tight or damaged
- NO-GO gauge enters more than 2 turns — thread is too loose
- Either failure condition = reject the part
Never force a gauge. Both plug gauges and ring gauges must be operated by hand pressure only. Using a wrench or excessive force will damage the gauge thread and invalidate your inspection results. If the GO gauge does not pass freely, the part fails — do not force it through.
Common Ordering and Inspection Mistakes
| Mistake | Consequence | How to Avoid |
|---|---|---|
| Ordering a plug gauge for an external thread | Wrong gauge — cannot inspect the part | Check internal vs external first |
| Ordering a ring gauge for an internal thread | Wrong gauge — cannot inspect the part | Check internal vs external first |
| Leaving out the tolerance class | Wrong gauge limits — may accept bad parts | Always state 6H or 6g (or 2B / 2A) |
| Confusing 6H (internal) with 6g (external) | Wrong gauge — opposite thread location | Uppercase = internal · Lowercase = external |
| Ordering GO ring only without NO-GO | Incomplete inspection — oversized threads pass | Always order full GO + NO-GO set |
| Forcing the GO gauge through | Gauge damage + false acceptance result | Hand pressure only — never use tools |
| Using a worn gauge without recalibration | Out-of-specification parts accepted | Calibrate every 6-12 months |
Frequently Asked Questions
Can I use a plug gauge to check an external thread?
No. A plug gauge is designed to enter an internal (female) thread. It cannot be used to inspect an external (male) thread. For external threads, you need a thread ring gauge.
What is the difference between 6H and 6g?
Both are ISO metric thread tolerance classes, but they apply to different thread locations. 6H (uppercase H) is for internal threads — nuts and tapped holes. 6g (lowercase g) is for external threads — bolts and shafts. The gauge limits are different and the two gauges are not interchangeable.
Do I need both GO and NO-GO gauges?
For complete production inspection, yes. The GO gauge checks that the thread is not too tight (minimum material condition). The NO-GO gauge checks that the thread is not too loose (maximum material condition). A thread can pass the GO and still fail the NO-GO — you need both to confirm the part is within tolerance.
What is a setting plug gauge?
A setting plug gauge (also called a master plug or reference plug) is used to set and verify adjustable thread ring gauges. It is not used to inspect workpieces — its purpose is to calibrate and reset the ring gauge to the correct dimension after wear or adjustment.
How do I know which size and tolerance to order?
Read the thread callout on the engineering drawing. It will show the nominal size, pitch, and tolerance class — for example M12×1.75-6H for an internal thread or M12×1.75-6g for an external thread. If the drawing does not specify a tolerance class, 6H (internal) and 6g (external) are the correct defaults for metric threads.
Can I get a calibration certificate with my gauge?
Yes. All GageTools thread plug gauges and ring gauges can include, on request, an ISO/IEC 17025 calibration certificate showing actual measured values for pitch diameter, major diameter, minor diameter, pitch, and thread angle —.
Not Sure Which Gauge to Order?
Send your thread callout or drawing — we will confirm the correct plug or ring gauge, tolerance class, and standard before production. Response within 24 hours.
Email RFQ 💬 WhatsAppRelated Buyer Guides
- What Is a Thread Plug Gauge? Sizes, Standards and How to Order
- What Is a Thread Ring Gauge? Sizes, Standards and How to Order
- GO/NO-GO Thread Gauge: Principle, Types and How to Use
✓ 20+ years gauge manufacturing
✓ ISO 9001:2015 certified
✓ In-house CNC grinding & inspection
✓ Drawing / RFQ reply within 24h
Have a drawing or thread callout ready? Request a thread gauge quote and our engineering team will review your specification.
Need gauges for this? GageTools makes GO/NO-GO thread plug and ring gauges with MOQ 1 piece: plug gauges from USD 20, ring gauges from USD 30, and standard stock sizes ship within 72 hours. Send your thread size for a quote.
Pingback: Thread Plug Gauge: GO/NO-GO Sizes, Standards & Ordering | GageTools