Thread Gauges / Internal Thread Inspection
GO/NO-GO Thread Plug Gauges Manufacturer
GO NO-GO plug gauges | Metric, UN, BSP, NPT | ISO, ANSI/ASME, DIN | Custom sizes
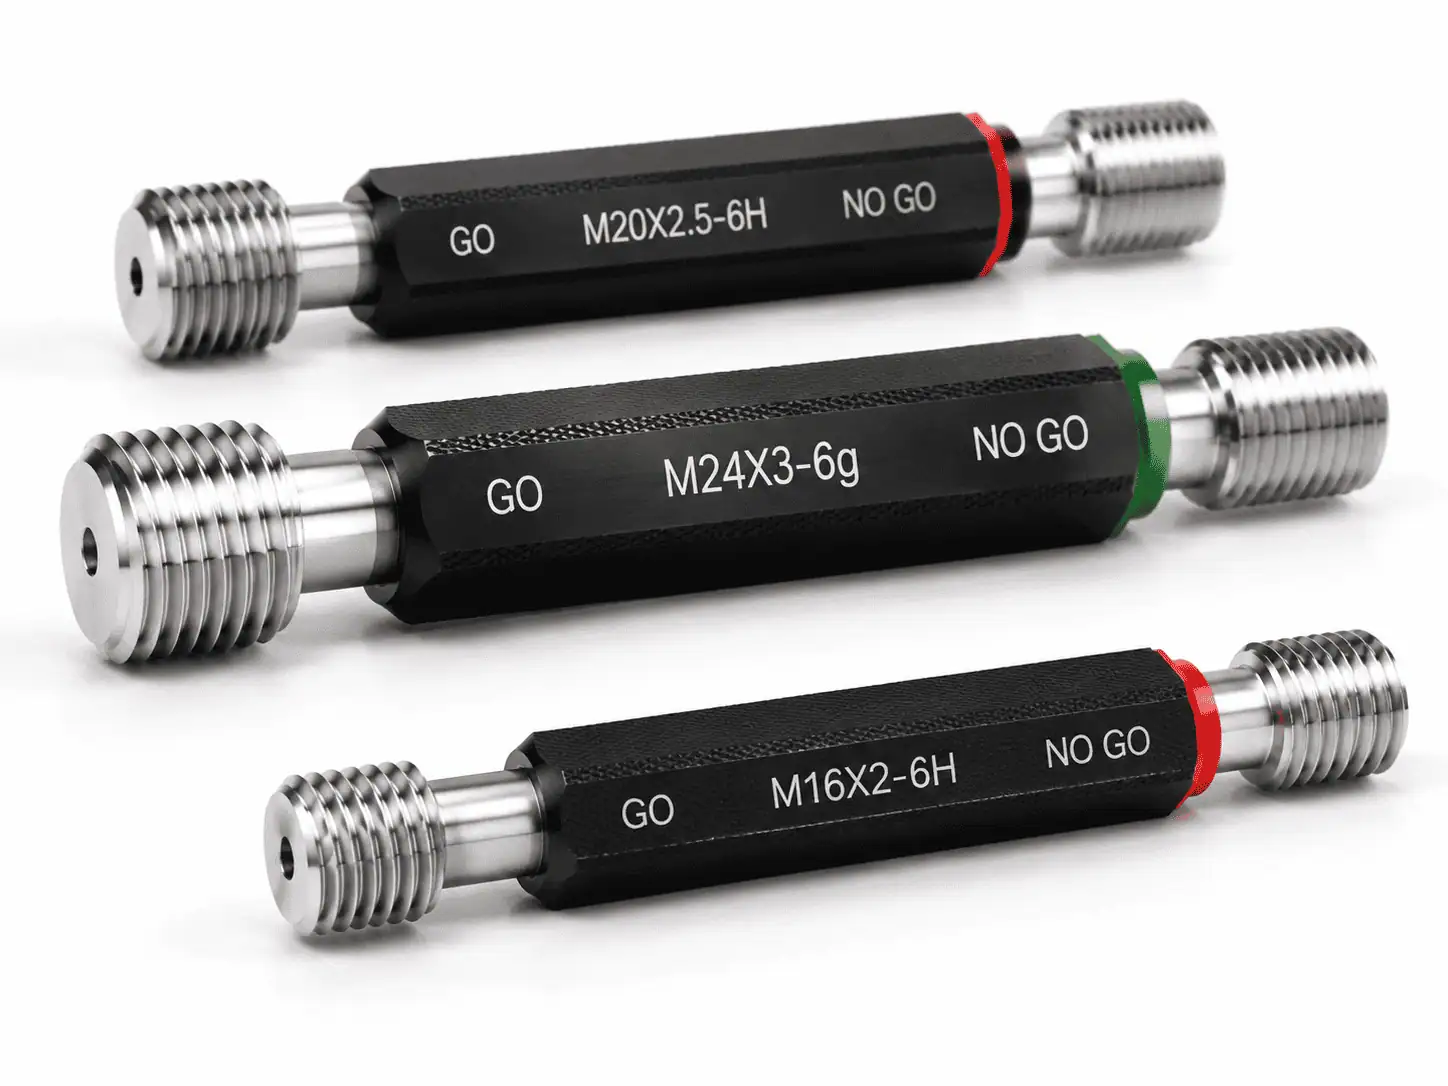
GageTools manufactures precision thread plug gauges for fast pass/fail inspection of internal threads in nuts, tapped holes, pipe fittings and machined components. Standard and custom GO/NO-GO plug gauges are available for global OEM buyers and distributors.
Final price depends on thread size, standard, class and quantity. Get an exact quote in 24 hours →
Inspection & Documentation
Our Inspection Room and Calibration Certificates
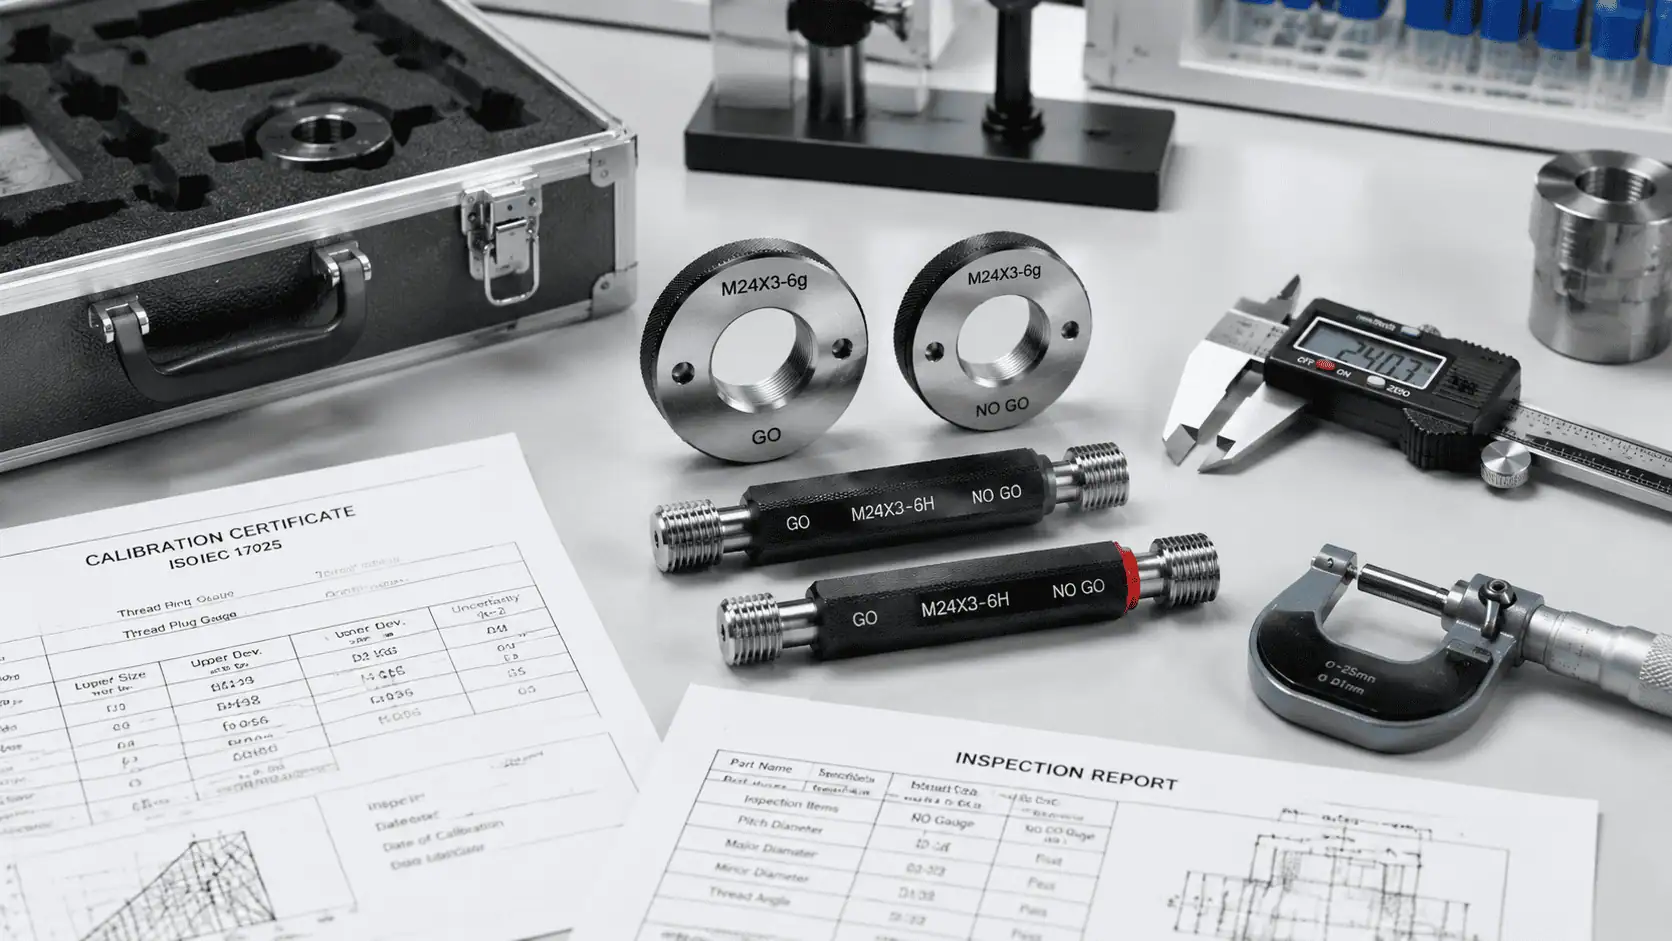
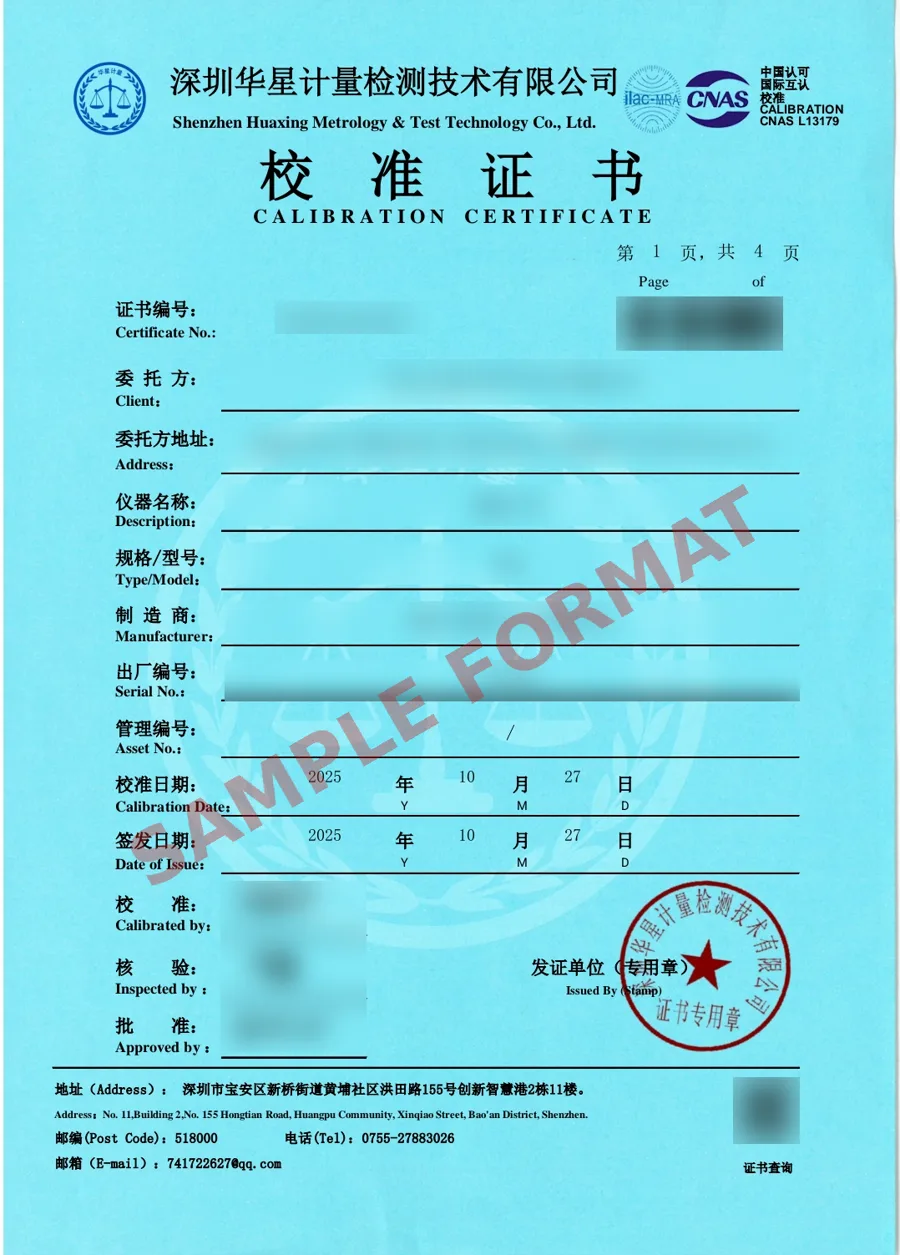
Gauges are checked in our inspection room before packing. When your order needs third-party traceability, we arrange calibration with a CNAS-accredited laboratory (ILAC-MRA signatory) and send the certificate with the gauges. Third-party CNAS calibration usually takes about 3 working days, so please mention it when you request a quote.
How it works
Thread Plug Gauges for Internal Thread Inspection
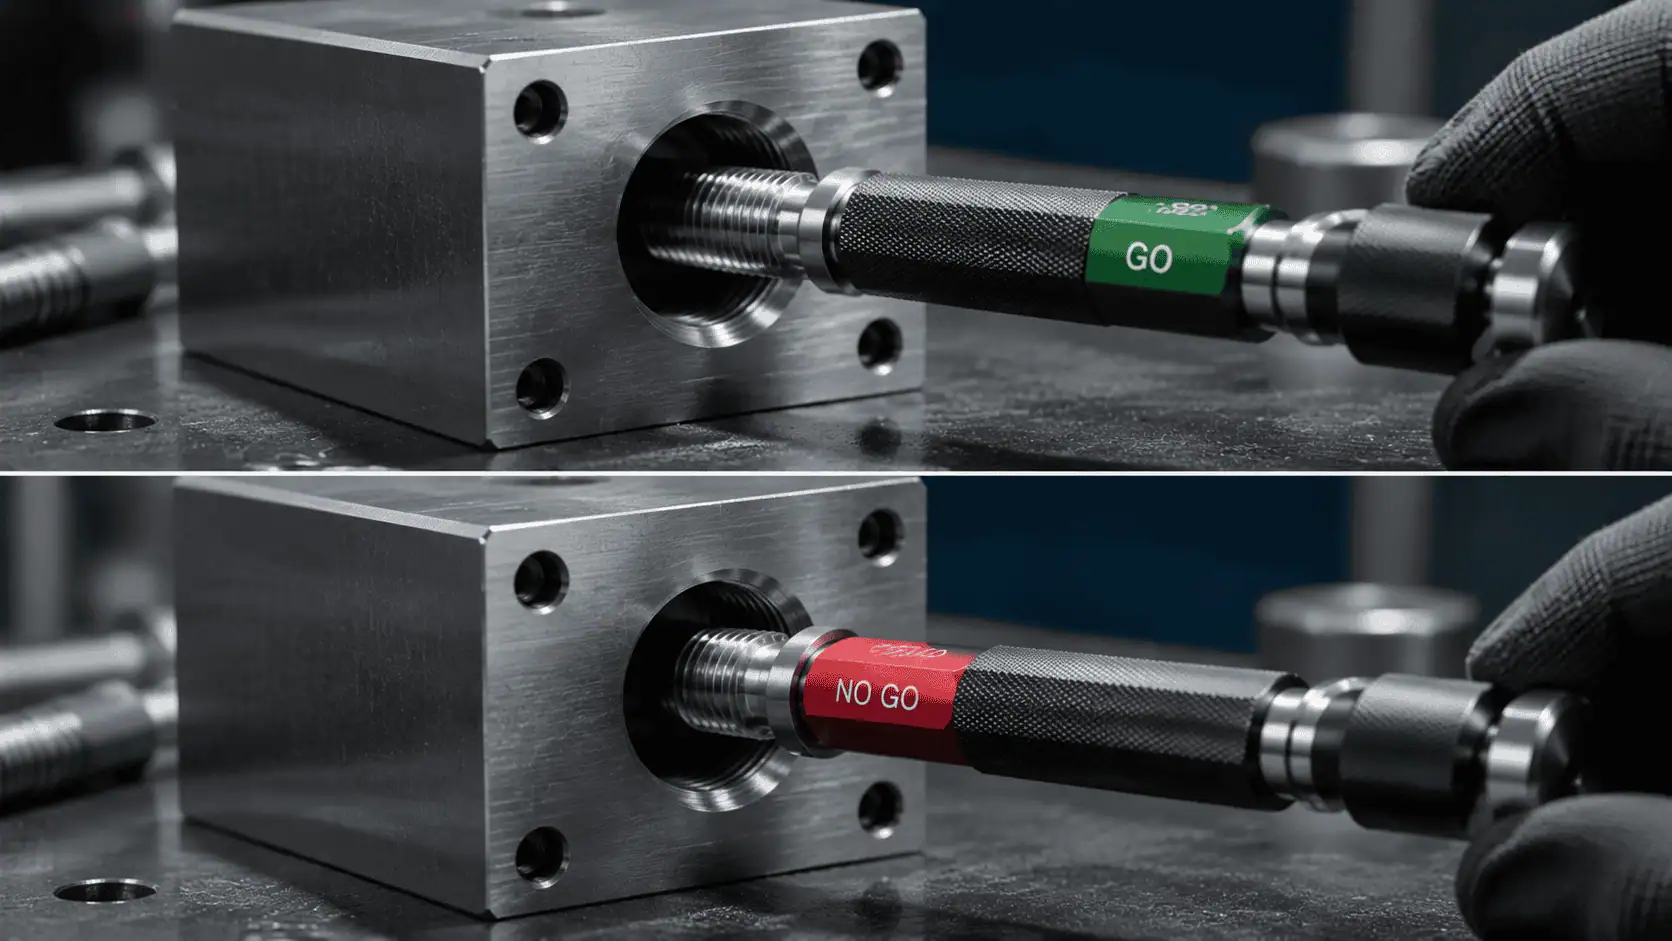
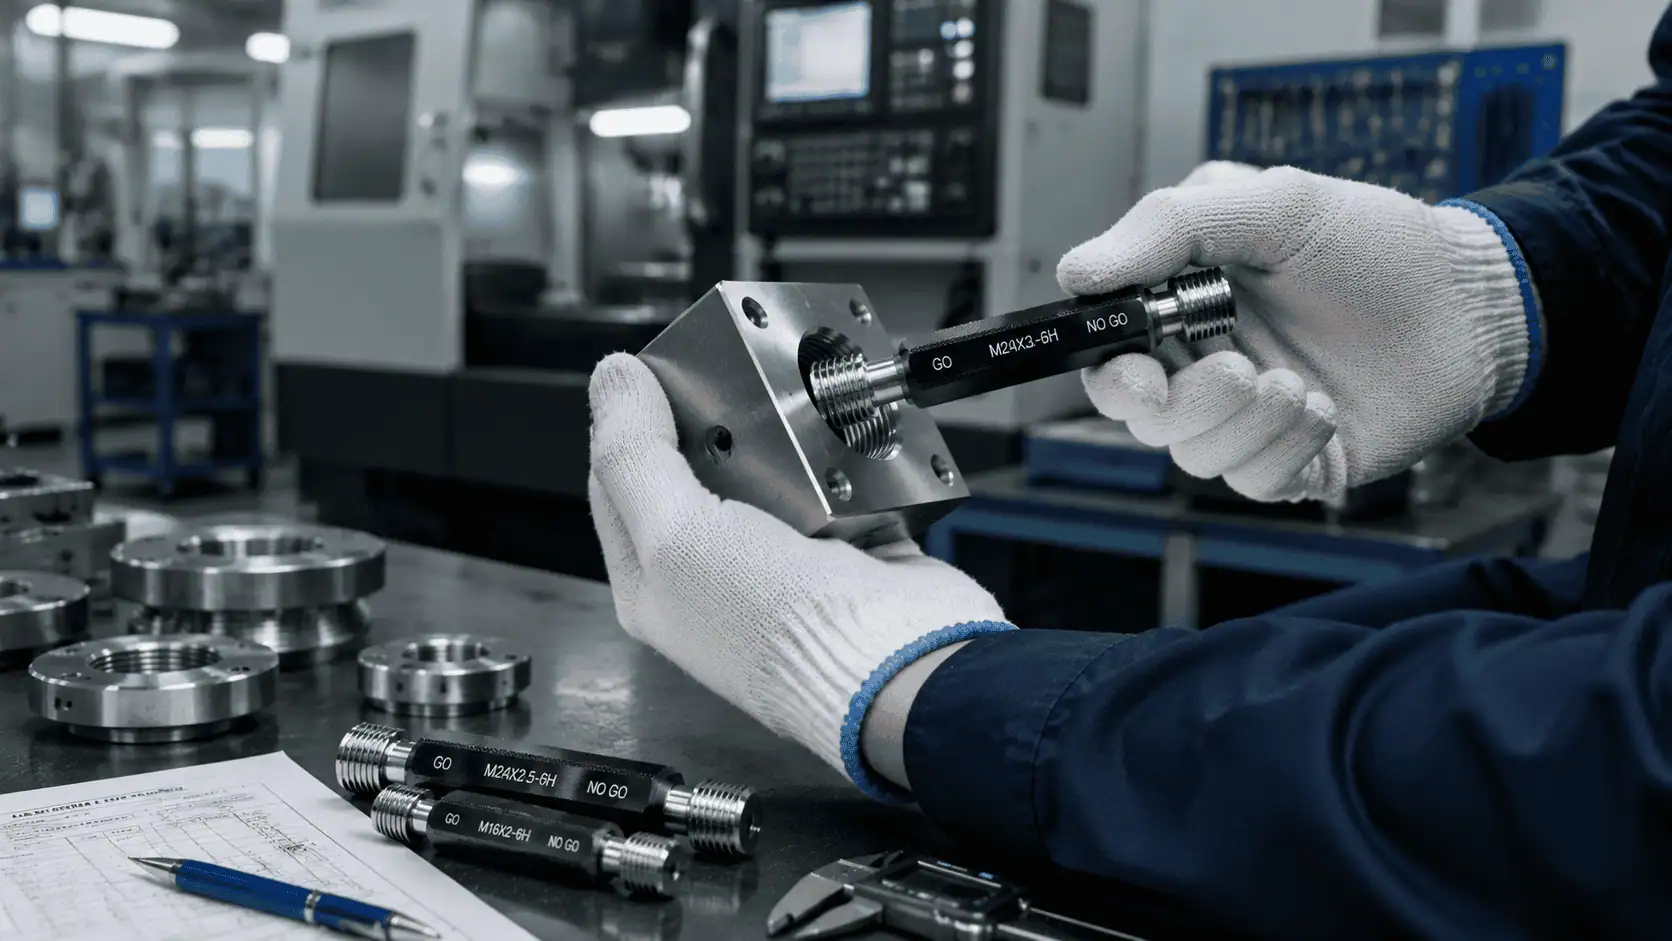
Thread plug gauges verify whether an internal thread is within the accepted tolerance zone. The GO member must thread through the full length under hand pressure only. The NO-GO member must not engage more than two turns. A part passes only when both conditions are met simultaneously.
- GO plug verifies thread is not too tight — checks all elements simultaneously
- NO-GO plug verifies thread pitch diameter is within the maximum material limit
- Pass/fail result in seconds — no thread wires or measuring instruments needed
- Suitable for production operators, incoming QC and final inspection
Applications
Used for Nuts, Tapped Holes and Machined Components
Thread plug gauges are specified in CNC machining, fastener production, automotive components, aerospace parts, hydraulic fittings and general mechanical assemblies across all major thread standards.
- Nuts, inserts and threaded bushings
- Blind holes and through holes in machined parts
- Pipe fittings, valves and fluid connectors
- OEM incoming inspection and production line checks
- Aerospace and automotive AS9100 / IATF 16949 applications
Plug Gauge Types
Standard and Custom Thread Plug Gauge Options
Choose the plug gauge design based on inspection workflow, thread depth, tolerance class and production volume.
Double-Ended GO/NO-GO Plug Gauges
Most common option for production line inspection. One handle carries both GO and NO-GO members, clearly marked with colour bands and engraved serial number.
- Compact and easy to use on production lines
- GO and NO-GO members clearly identified — colour coded
- Metric, UN, BSP, NPT and custom thread forms
- Standard for sizes M1–M60 and #0–1½” UN
Single-Ended / Separate Member Gauges
Used for larger diameters, deep-reach designs, or when GO and NO-GO must be separately controlled in a calibrated inspection environment.
- Standard for sizes above M60 / 1½” UN
- Custom handle length and marking options
- Individual serial numbers on each member
- Calibration certificate covers each member separately
Specifications
Common Thread Plug Gauge Specifications
Use this table as a quick RFQ guide. If your thread is not listed, send the standard, size, pitch, tolerance class and drawing — we confirm in 24 hours.
| Thread System | Common Sizes | Tolerance / Class | Plug Gauge Type | Typical Application |
|---|---|---|---|---|
| Metric ISO | M1–M100, coarse and fine pitch | 4H · 5H · 6H · 7H | GO / NO-GO / Double-ended | General machining, nuts, tapped holes |
| UN / UNC / UNF | #0 to 4″, standard and fine | 1B · 2B · 3B | GO / NO-GO / Set | North American OEM and aerospace components |
| BSP / BSPP / BSPT | G 1/8″ to G 4″ · Rc 1/8″ to Rc 4″ | ISO 228 / ISO 7 | Parallel or taper plug gauge | Pipe fittings, valves, hydraulics |
| NPT / NPTF | 1/16″ to 4″ | L1 · L2 · L3 | Taper plug gauge | Oil, gas, hydraulic and pneumatic fittings |
| ACME / Trapezoidal | Standard and custom | 2G · 3G · 7H | Special plug gauge | Lead screws, motion systems, machinery |
| UNJ (Aerospace) | #0 to 4″ | 3B UNJ | UNJ plug gauge | Aerospace fasteners per MIL-S-8879 |
→ For complete pitch diameter limits by size, see Metric Thread Plug Gauge Size Chart M1–M100
Quality and Certification
ISO/IEC 17025 Calibration Certificate — Available on Request
Every thread plug gauge from GageTools can be supplied, on request, with a full ISO/IEC 17025 calibration certificate. The certificate shows actual measured values for all critical dimensions — not just a conformance statement.
- Actual measured pitch diameter — GO and NO-GO members, compared against upper and lower limits
- Actual measured major diameter, minor diameter, pitch and thread angle
- Measurement uncertainty stated — k=2, 95% confidence
- NIST-traceable calibration chain — verified through accreditation body registry
- Unique engraved serial number on every gauge — for calibration history traceability
- Inspector and approver signatures — meets AS9100, IATF 16949 and ISO 9001 audit requirements
→ How to Read a Thread Gauge Calibration Certificate
→ Thread Gauge for Aerospace: AS9100 and NIST Traceability Guide
Why GageTools
Thread Plug Gauges for OEM Buyers and Distributors
Direct manufacturer — no middleman. Every gauge CNC ground, lapped and calibrated in-house.
In-House CNC Grinding
All thread plug gauges are ground on our own CNC grinding machines — no subcontracting. Full control over dimensional accuracy from raw material to final calibration.
Standard or Made to Drawing
Common metric and inch plug gauges available from stock. Special gauges produced from drawings, samples or customer standards. MOQ 1 piece for custom sizes.
Global Export Ready
DHL Express / FedEx / UPS shipping with tracking. Standard sizes ship in 72 hours. Custom gauges in 5–15 working days. Export documentation included.
Ordering Guide
What to Send for a Fast Quote
A complete specification gets a response with price, lead time and certificate options within 24 hours.
1. Thread Details
Thread system, size, pitch, standard and tolerance class — e.g. M12×1.75 6H or 1/4-28 UNF 3B. For custom threads, attach a DXF or PDF drawing.
2. Gauge Requirement
GO plug, NO-GO plug or complete GO/NO-GO set. Double-ended or single-ended. Any special marking, handle or packaging requirements.
3. Quantity and Delivery
Order quantity, delivery country and target delivery date. ISO/IEC 17025 calibration certificate available on request — no need to request it separately.
Plug Designs
Thread Plug Gauge Designs: Taperlock, Trilock, Reversible and Double-Ended
The gauging member is what checks the thread, but the handle design affects cost, replacement and handling on the shop floor. The right choice depends mainly on diameter and on how quickly your GO members wear.
| Design | How it works | Best suited to |
|---|---|---|
| Taperlock | Gauging member has a tapered shank pressed into the handle | Smaller diameters; worn members replaced without a new handle |
| Trilock | Member is held on the handle by locking prongs and a screw | Larger diameters where a taper shank is impractical |
| Reversible | Member can be flipped so the unused end becomes the gauging face | High-volume lines where the GO end wears quickly |
| Double-ended | GO member on one end, NO-GO on the other, one handle | Everyday inspection where both checks are made at the bench |
Separate GO and NO-GO gauges on individual handles are also available where inspectors prefer colour-coded or clearly separated members, or where one member wears out much faster than the other. Tell us which design your inspectors already use so replacement members fit your existing handles. For help choosing between plugs and rings, see thread plug gauge vs ring gauge.
Blind Holes
Blind Holes and Depth-Marked Plug Gauges
In a blind hole, a GO plug can enter freely yet still stop short of the depth the drawing requires, because tap chamfer and chips reduce full-thread length at the bottom. A standard plug confirms size but not depth. A depth-marked plug adds a groove or step at the minimum full-thread depth, so the inspector can see whether the GO member reaches it.
- Give the minimum full-thread depth and the drilled hole depth from the drawing.
- State whether the depth is measured from the part face or from a counterbore.
- Keep the GO member length short enough to clear the drill point.
- Clean chips out before gauging, or the plug will stop early.
Depth markings are specified on the gauge data sheet and approved with the thread dimensions, so the same plug can be reordered for the same part without a new review.
More detail is in thread gauges for blind holes.
Wear Signs
Signs a Thread Plug Gauge Is Worn
GO plugs wear with every part they check, and a worn GO plug starts to accept holes that are too small. Watch for these signs between calibrations:
| Sign | What it suggests | Action |
|---|---|---|
| Passed holes are hard to assemble with mating bolts | GO plug may be undersize from wear | Check the gauge before releasing more parts |
| Bright bands, burrs or flattened crests on leading threads | Local wear or damage on the first threads | Remove from use and inspect |
| GO plug turns in much easier than a new plug | Pitch diameter reduced | Measure pitch diameter |
| Calibration result near the wear limit | Little service life left | Order a replacement member now |
Replace or re-certify the gauge once it reaches the wear limit. See thread plug gauge wear limits.
FAQ
Thread Plug Gauge Questions
Can you supply only the replacement GO member instead of a full plug gauge?
Yes, for taperlock and trilock designs. Send the thread callout, class and handle design, or a photo of the existing handle, and we will supply a replacement gauging member to fit it. This is usually cheaper than a complete new gauge and keeps your inspectors using familiar handles.
Why does the NO-GO plug last longer than the GO plug?
The GO plug is screwed fully through every good part, so its flanks rub on the entire thread length each time. The NO-GO plug should enter no more than a couple of turns on good parts, so it sees much less contact. That is why GO members are replaced more often.
How short can a plug gauge be for a shallow blind hole?
The GO member can be made shorter than standard to suit the hole, provided it still covers the required thread engagement length. Send the minimum full-thread depth and the drilled depth, and we will propose a member length and any depth marking in the data sheet before production starts.
Should the NO-GO plug be checked for wear too?
Yes. It wears more slowly, but it still loses size over time, and a worn NO-GO plug can enter oversized holes and let them pass. Include both members in your calibration schedule, and replace the NO-GO when its pitch diameter reaches the permitted limit.
What does a thread plug gauge inspect?
A thread plug gauge inspects internal threads — tapped holes, nuts and threaded fittings — to confirm the thread pitch diameter is within the specified tolerance class (e.g. 6H). The GO member checks the minimum material condition; the NO-GO member checks the maximum.
What is a GO/NO-GO plug gauge set?
A complete set includes a GO member that must thread through the full hole length under hand pressure only, and a NO-GO member that must not engage more than two turns. Both results together determine whether the part passes or fails.
What tolerance class should I order?
For metric internal threads, 6H is the standard default for general engineering. Use 4H or 5H for aerospace or precision applications. Use 7H for parts that will be zinc plated after tapping. If no class is shown on the drawing, 6H is correct. See our Tolerance Classes Guide for full details.
Can the gauge be supplied with a calibration certificate?
Yes — ISO/IEC 17025 calibration certificate available on request for every thread plug gauge. The certificate shows actual measured values for pitch diameter, major diameter, minor diameter, pitch and thread angle. NIST-traceable. Accepted by ISO 9001, IATF 16949 and AS9100 auditors.
Can you make custom plug gauges?
Yes. We manufacture custom thread plug gauges from DXF or PDF drawings. Any thread form, non-standard pitch, proprietary tolerance class or special handle design. MOQ 1 piece. Send your drawing for a quotation within 24 hours.
What is the minimum order quantity and lead time?
MOQ is 1 set for both standard and custom gauges. Standard metric and UN plug gauge samples ship within 72 hours by DHL Express. Custom gauges ship in 5–15 working days after drawing approval. All orders can include, on request, the calibration certificate.
Get a Quote
Request Thread Plug Gauge Price
Send your thread specification or drawing. We reply with price, lead time, certificate confirmation and shipping options within 24 hours.
Quick RFQ
Use these links to send a structured inquiry with your thread size, tolerance class, quantity and delivery country.