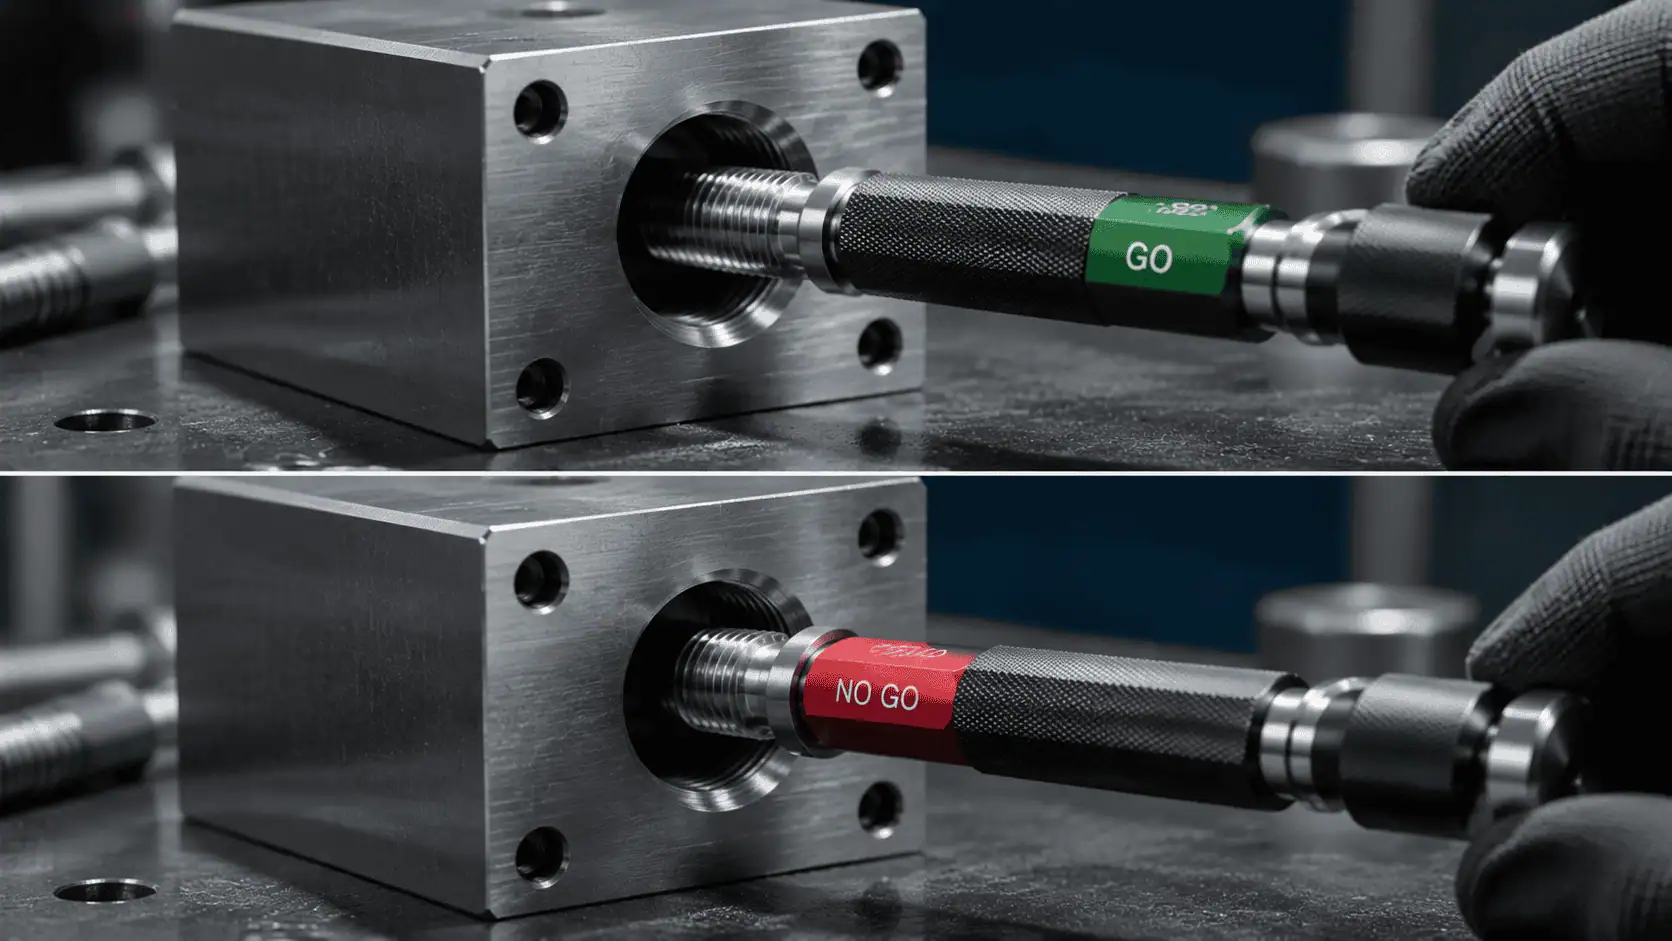
Need gauges for this? GageTools manufactures GO/NO-GO thread plug gauges and thread ring gauges in Dongguan, China. Standard sizes ship from stock within 72 hours, MOQ is 1 piece, and every RFQ gets a reply within 24 hours — request a quote.
Tools You Need
- Digital or dial calipers
- Metric and inch thread pitch gauges (with 55° and 60° leaves if possible)
- A magnifier or loupe for small threads
- A thread reference chart (metric, UN, BSP, NPT)
The Five Checks, Step by Step
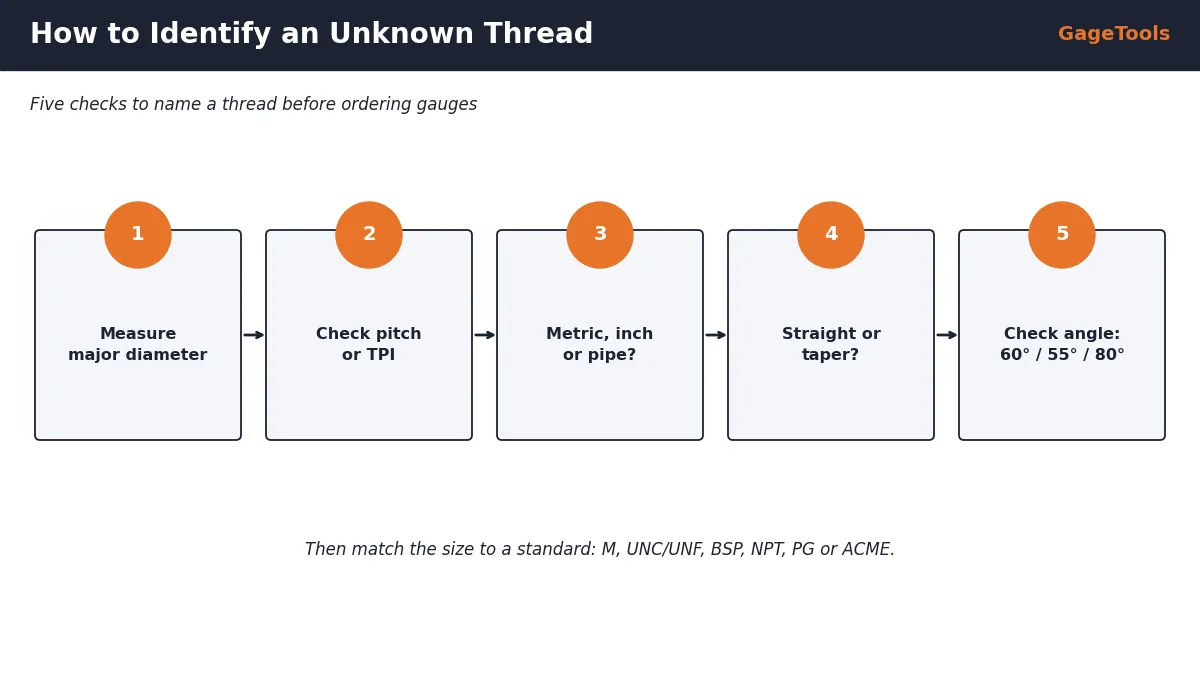
- Measure the major diameter. On an external thread, measure across the crests. On an internal thread, measure the bore at the crests or use a known bolt. Expect the reading to be slightly under nominal on bolts.
- Find the pitch or TPI. Try metric and inch pitch gauge leaves until one sits cleanly with no light between the teeth. Or measure across 10 threads and divide.
- Decide metric, inch or pipe. A clean fit on a metric leaf (e.g. 1.5 mm) means metric; on an inch leaf (e.g. 13 TPI) means UN or Whitworth. A diameter much larger than the nominal size suggests a pipe thread (BSP or NPT).
- Check for taper. Measure the diameter at both ends of the thread. A difference means a taper thread such as NPT, BSPT or API.
- Confirm the flank angle. 60° for metric, UN and NPT; 55° for BSW, BSF and BSP; 80° for PG; 29°/30° trapezoidal for ACME and Tr.
Quick Match Table
| What you find | Likely thread | Gauge to order |
|---|---|---|
| 60°, metric pitch, straight | ISO metric (M) | Metric 6H / 6g gauges |
| 60°, TPI, straight | UNC / UNF / UNEF | UN 2B / 2A gauges |
| 60°, TPI, tapered | NPT / NPTF | L1 taper plug / ring |
| 55°, TPI, straight, pipe size | BSPP (G) | BSPP plug / ring |
| 55°, TPI, tapered, pipe size | BSPT (R / Rc) | BSPT taper gauges |
| 55°, TPI, straight, bolt size | BSW / BSF | Whitworth gauges |
| 80°, shallow, straight | PG conduit | PG gauges |
| 29° / 30° trapezoid | ACME / Trapezoidal (Tr) | ACME or Tr gauges |
Threads That Are Easy to Mix Up
| Pair | How to tell them apart |
|---|---|
| 1/4-20 UNC vs M6x1 | 1/4″ is 6.35 mm; M6 is 6.0 mm, and 20 TPI ≠ 1.0 mm pitch |
| 3/4-16 UNF vs M18x1.5 | Pitch 1.588 mm vs 1.5 mm — try both leaves |
| 1/2″ BSPP vs 1/2″ NPT | 55° and straight vs 60° and tapered |
| 1/4″ BSW vs 1/4-20 UNC | Same TPI, but 55° vs 60° angle |
| M12x1.5 vs M12x1.25 | Both fine M12; check pitch carefully |
Near-miss threads cause the worst problems. A 3/4-16 UNF fitting can start in an M18x1.5 port and then gall or leak. Always confirm pitch and angle, not just diameter.
When the Thread Matches No Standard
Some parts use special threads: non-standard diameters, special pitches, modified forms or old company standards. In that case we can work from a sample part, a worn gauge, or your measurements to reverse-engineer the thread and make matching GO/NO-GO gauges. See replacing a gauge without a drawing.
Identifying an Internal Thread (Nut or Tapped Hole)
Internal threads are harder to measure because you cannot reach the crests easily. These methods help:
- Use a known bolt: if a standard bolt screws in smoothly by hand, the thread is probably the same size and pitch. Confirm with the pitch gauge on the bolt.
- Measure the minor diameter: use calipers inside the hole across the crests of the internal thread; compare with tap drill tables.
- Take an impression: for larger holes, a thread impression compound or a cast shows the profile and pitch.
- Try GO plug gauges of candidate sizes: only if you already have them — never force a gauge.
Recognising Pipe Threads
Pipe thread sizes are named after nominal bore, not outside diameter, so a “1/2 inch” pipe thread measures about 21 mm across the threads. If your measurement is much larger than the name would suggest, you are almost certainly looking at a pipe thread.
| Nominal size | Approx. OD (mm) | NPT TPI | BSP TPI |
|---|---|---|---|
| 1/8″ | 10.3 | 27 | 28 |
| 1/4″ | 13.6 | 18 | 19 |
| 3/8″ | 17.1 | 18 | 19 |
| 1/2″ | 21.3 | 14 | 14 |
| 3/4″ | 26.7 | 14 | 14 |
| 1″ | 33.4 | 11.5 | 11 |
1/2″ and 3/4″ NPT and BSP both have 14 TPI. For these sizes, check the angle (60° vs 55°) and the taper — pitch alone cannot tell them apart.
Record What You Found
Once identified, write the full designation on the drawing or work instruction, including the class if it is known. This saves the next person from repeating the process and makes gauge ordering straightforward.
| Field | Example |
|---|---|
| Thread designation | M18x1.5 / 3/4-16 UNF / G 1/2 |
| Internal or external | Internal (port) |
| Class | 6H / 2B / A |
| Length or depth | 15 mm full thread |
| Notes | Plated after machining |
Special and Non-Standard Threads
| Type | How it differs | How to recognise |
|---|---|---|
| Special diameter / pitch | Standard form, unusual combination | Diameter and pitch match no table |
| Modified class | Standard size, special limits | Drawing shows special tolerances |
| Multi-start threads | Two or more thread starts | Lead is a multiple of pitch; several thread ends visible |
| Buttress threads | Asymmetric flanks (e.g. 7°/45°) | One steep and one sloping flank |
| Company standards | Old in-house threads | Found on legacy machines |
All of these can be gauged. Special threads simply need the gauge to be designed from a drawing, specification or sample rather than a standard table.
Taking Photos That Help Identification
- Photograph the thread side-on, with a ruler or calipers in the frame.
- Include a close-up with a pitch gauge leaf sitting in the thread.
- Show both ends of the thread to reveal any taper.
- Add a photo of the whole part so its function is clear.
- Note any markings on the part or the drawing number.
Identifying Trapezoidal and ACME Threads
Power-transmission threads on lead screws, vices and jacks are usually ACME (inch, 29°) or Trapezoidal (metric, 30°). They have flat crests and roots and a much deeper, wider profile than fastening threads.
| Feature | ACME | Trapezoidal (Tr) |
|---|---|---|
| Angle | 29° | 30° |
| Units | Inch (TPI) | Metric (pitch in mm) |
| Example | 1-5 ACME-2G | Tr20x4-7H |
| Standard | ASME B1.5 | ISO 2901–2904 / DIN 103 |
A 1-5 ACME and a Tr24x5 can look alike. Measure pitch in both inches and millimetres, and check the angle, before ordering gauges.
Once Identified: Finding the Class
Knowing the thread size is only half the job. To order the correct gauge you also need the tolerance class. Look for it on the drawing, on the mating part’s specification, or on an existing gauge. If none is available:
Summary
Identifying a thread comes down to five facts: diameter, pitch, system, taper and angle. With calipers, a pitch gauge set and the quick match table, most threads can be named in minutes. Watch out for look-alikes such as 3/4-16 UNF and M18x1.5, or 1/2″ BSPP and 1/2″ NPT. When a thread matches no standard, a sample part, old gauge or drawing is enough for us to identify it and make matching GO/NO-GO gauges.
Key Terms
Quick definitions of the terms used in this guide:
| Term | Meaning |
|---|---|
| Major diameter | Largest diameter of the thread |
| Minor diameter | Smallest diameter of the thread |
| Pitch / TPI | Thread spacing in mm / threads per inch |
| Flank angle | Included angle of the thread profile |
| Taper thread | Thread whose diameter changes along its length |
| Nominal bore | Size name used for pipe threads |
| Multi-start | Thread with more than one helix |
Practical Tip: Keep Reference Bolts
A small box of known-good bolts and nuts in common metric, UNC, UNF and BSP sizes is one of the most useful identification tools in any workshop. Trying a reference bolt in an unknown hole is often faster than measuring.
Not Sure What Thread You Have?
Send a sample, photos with a ruler, or your measurements. We identify the thread and quote the correct GO/NO-GO gauges.
Related: Pipe thread comparison · UNC vs UNF vs UNEF · Metric thread chart
Frequently Asked Questions
✓ 20+ years gauge manufacturing
✓ ISO 9001:2015 certified
✓ In-house CNC grinding & inspection
✓ Drawing / RFQ reply within 24h
Send Us Your Thread — We Will Identify It
GageTools identifies unknown and special threads from samples or measurements and makes matching GO/NO-GO gauges. ISO/IEC 17025 calibration certificate available on request. Standard sizes ship from stock within 72 hours; custom gauges in 10–15 working days. MOQ 1 piece. WhatsApp for fastest response.
💬 WhatsApp Quote 📐 Send Drawing for Quote