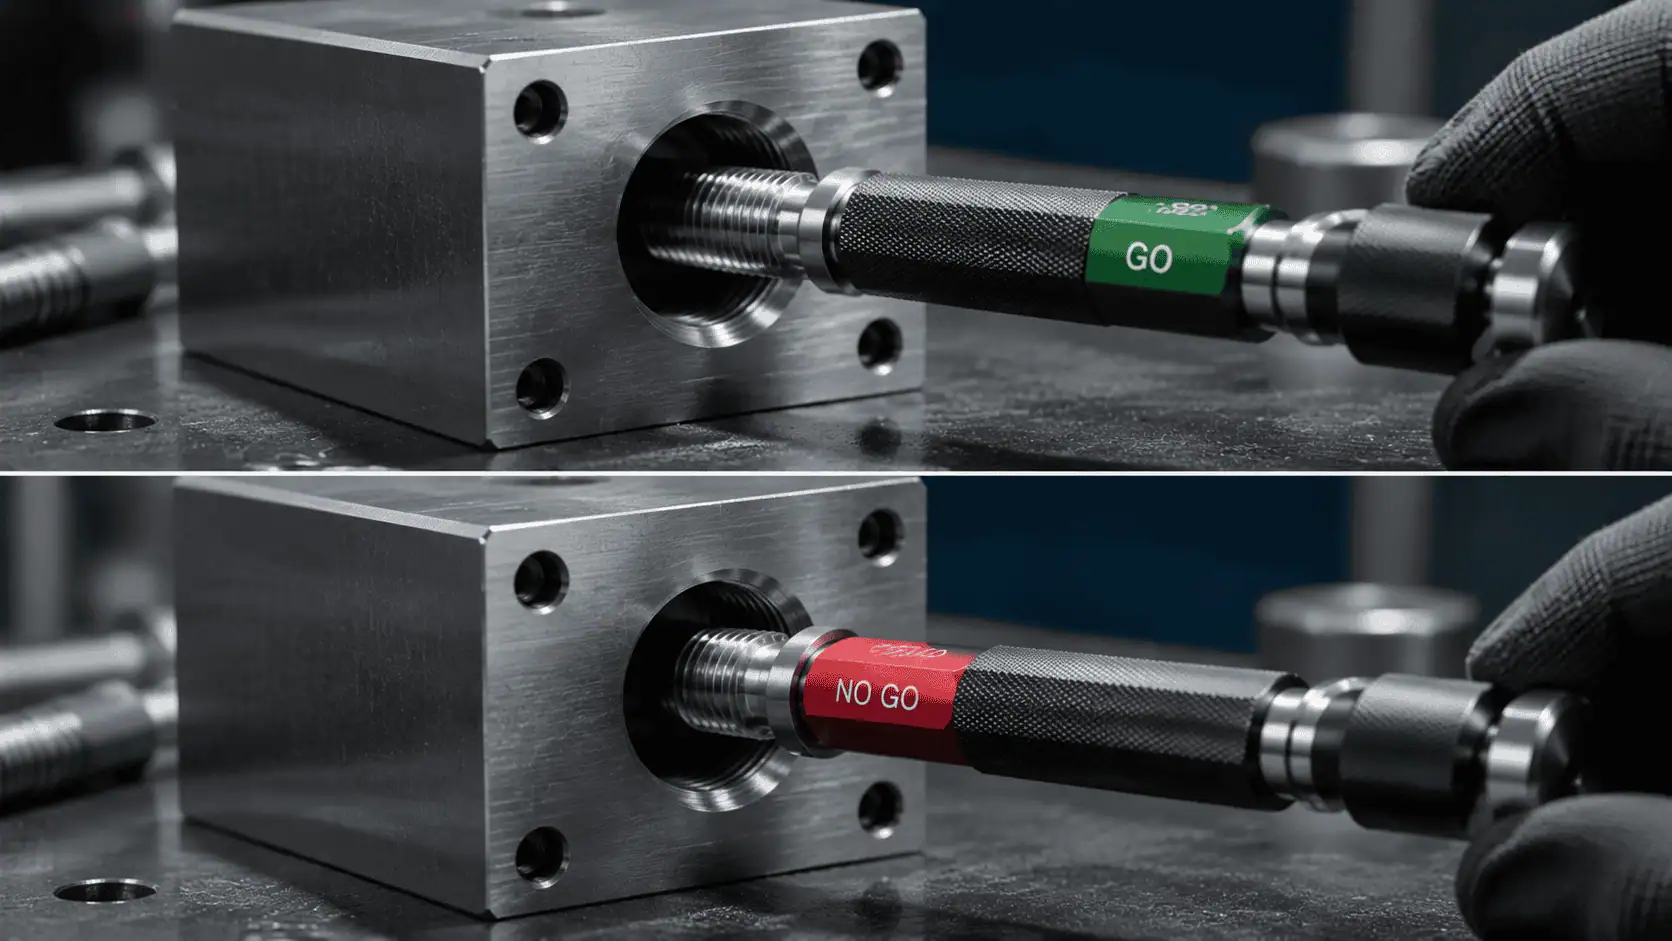
Need gauges for this? GageTools manufactures GO/NO-GO thread plug gauges and thread ring gauges in Dongguan, China. Standard sizes ship from stock within 72 hours, MOQ is 1 piece, and every RFQ gets a reply within 24 hours — request a quote.
The Typical Dispute: Accepted at Shipping, Rejected at Receiving
A batch of tapped housings leaves the supplier with a clean final inspection record. At the customer’s receiving dock the same parts are checked again, and the GO plug gauge will not enter, or the NO-GO plug goes in too far. The lot is rejected, a non-conformance report is raised, and both sides are sure their gauge is right.
Often both sides are right: both gauges are calibrated and within tolerance. The problem is a borderline part meeting two gauges that sit at slightly different points inside the permitted gauge tolerance.
Why Two Calibrated Gauges Can Give Different Results
A GO/NO-GO thread gauge is itself a manufactured part. Standards such as ISO 1502 for metric threads and ASME B1.2 for unified inch threads give each gauge a small manufacturing tolerance, and the GO member also has a wear allowance. A new GO plug and a GO plug that has worn close to its limit are both acceptable gauges, yet they are not the same size.
Other factors add to the gauge-to-gauge difference:
- Form and lead. The full-form GO gauge checks functional size, so small lead or form differences between gauges matter on imperfect threads.
- Temperature. Warm parts straight off the machine do not gauge like parts at room temperature.
- Cleanliness. Chips, coolant, burrs and plating flakes make a GO gauge feel tight.
- Technique. Different hand torque or NO-GO turn counting changes borderline decisions.
- Coating. A part checked before plating and again after plating is effectively a different part.
First Checks Before Anyone Blames a Gauge
Most disputes end once both sides confirm the basics.
| Check | What to confirm | Typical finding |
|---|---|---|
| Thread designation | Same size, pitch and class on both gauges | Customer using 6H gauge, supplier using 6G, or 2B vs 3B |
| Gauge identity | GO and NO-GO serial numbers and marking | Wrong member picked up, or gauges from different sets mixed |
| Calibration status | Both gauges in date, with results available | One gauge overdue or last result near the wear limit |
| Coating condition | Before or after plating, and which gauge applies | Pre-plate gauge used on plated parts |
| Part condition | Clean, deburred, at room temperature | Burr at the first thread or coolant in the hole |
| Gauging method | Hand pressure, full length for GO, turn count for NO-GO | GO forced with a tommy bar, or NO-GO turns counted from the wrong start |
Class mix-ups are more common than people expect. For internal metric threads the GO plug is the same for 4H, 5H, 6H and 7H because the fundamental deviation of the H position is zero; only the NO-GO plug changes with the tolerance grade. For the G position the GO gauge itself is different. So a customer using a 6G GO plug on a 6H thread, or a supplier using a 7H NO-GO on a 6H callout, will get results that cannot be reconciled until the right gauges are used. See our guide to 6G vs 6H thread tolerance for the detail.
Do not re-adjust or “ease” a gauge to end a dispute. Loosening an adjustable ring on the shop floor, or lapping a GO plug until the parts pass, destroys the gauge’s traceability and hides the real problem in the process.
Measure Pitch Diameter Instead of Arguing
GO/NO-GO gauges give a decision, not a number. Once two gauges disagree, get variable data on the disputed parts. The key characteristic is pitch diameter, because that is what the NO-GO member checks and what drives most GO failures.
- External threads: three-wire measurement with a calibrated micrometer or a measuring machine gives simple pitch diameter directly.
- Internal threads: pitch diameter is harder to measure directly. Options include thread comparators, internal thread measuring machines, or sectioning a sample part for optical measurement.
- Functional size: if pitch diameter is inside the limits but the GO gauge still will not enter, the problem is lead, flank angle or form, which a full-form GO gauge detects and a pitch diameter measurement alone does not.
Measure several parts across the lot. Results clustered near a limit confirm a borderline process; results clearly inside the limits point to the rejecting gauge, which should go for calibration.
Compare the Two Gauges’ Calibration Certificates
Ask both sides for the latest calibration certificate of each gauge involved. A certificate that only says “pass” is of limited use in a dispute. You want the measured values, so you can see where each gauge sits inside its tolerance. Our guide on how to read a thread gauge calibration certificate covers the fields to look for.
| Certificate item | Why it matters in a dispute |
|---|---|
| Measured pitch diameter | Shows where each gauge sits within its gauge tolerance or wear limit |
| Major and minor diameters | Confirms the gauge form is correct, not only the pitch diameter |
| Measurement uncertainty | Tells you how much the stated value can be trusted |
| Reference standard and traceability | Confirms the measurement links back to national standards |
| Calibration date and due date | Confirms the gauge was valid on the day the parts were checked |
| Laboratory accreditation | An ISO/IEC 17025 accredited result is easier for both sides to accept |
Using a Referee Gauge to Settle the Result
A referee gauge is a gauge set that both parties agree in advance will make the final decision when their working gauges disagree. It is not a special gauge type; it is an organisational agreement. What matters is that it is calibrated, kept out of daily production, and recorded.
- Same designation and class as the drawing
- Recent calibration with measured values on the certificate
- Stored separately, not used in production
- Held by the customer, the supplier or a third-party lab as agreed
- Used with a written method: hand pressure, clean parts, room temperature
Once both sides accept that the referee set decides, a borderline lot is gauged once with it and the result stands.
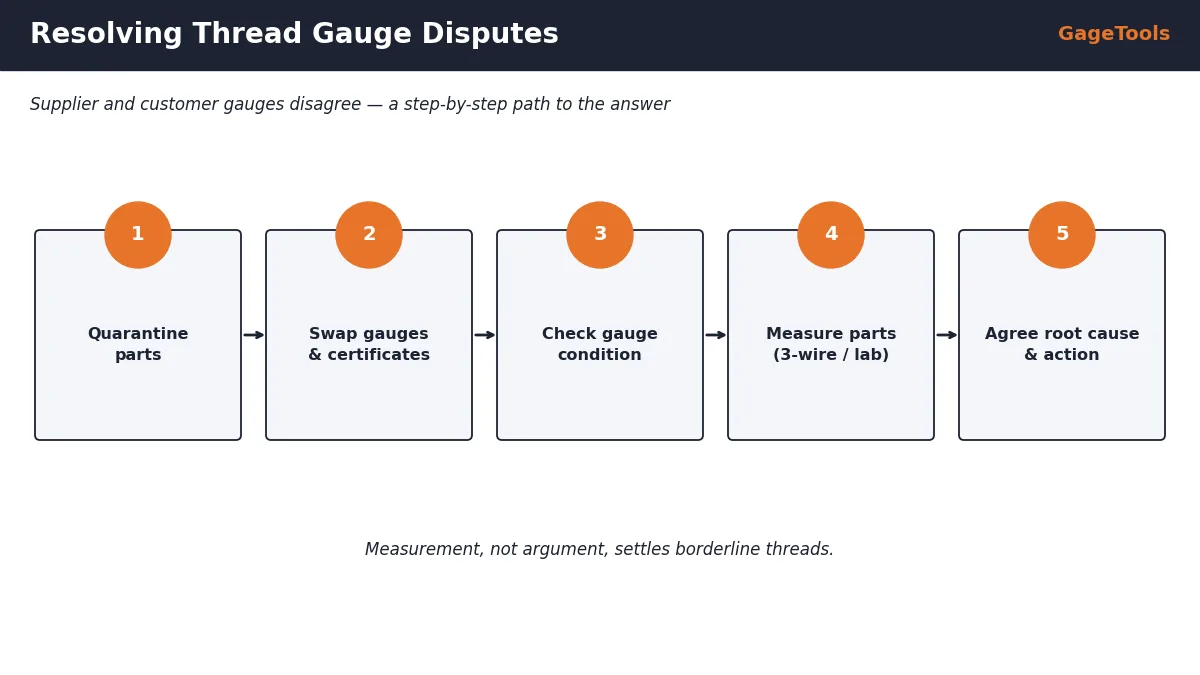
A Step-by-Step Dispute Resolution Process
- Contain. Quarantine the disputed lot and the supplier’s remaining stock.
- Exchange information. Share gauge serial numbers, designations, certificates and the exact reject description.
- Swap samples. Check the same parts on both sides’ gauges.
- Measure. Get pitch diameter data on a sample of disputed parts.
- Decide with the referee. Where parts remain borderline, the agreed referee gauge or lab decides.
- Correct. Recalibrate or replace any gauge found outside its limits; centre the process if parts are near a limit.
- Document. Close the NCR with the root cause and update the quality agreement if a gap was found.
Write Gauging Into the Quality Agreement
Most repeated disputes come from things nobody wrote down. A short gauging section in the supplier quality agreement or on the drawing prevents them. It should cover:
- The thread standard and gauging system that applies, for example ISO 1502 for metric threads or ASME B1.2 with a gauging system from ASME B1.3 for unified threads.
- Whether threads are gauged before or after plating or coating, and which gauges apply at each stage.
- The calibration requirements for gauges on both sides, including interval and whether certificates must show measured values.
- The referee method: which gauge set or laboratory decides when working gauges disagree.
Some customers ask suppliers to buy gauges to the same specification as their receiving gauges. If you are changing sources, see our guide on switching thread gauge manufacturers.
What to Send When Ordering Gauges to Resolve a Dispute
If a dispute shows that you need new working gauges, a referee set, or gauges matched to your customer’s, send us the following so we can quote the right GO/NO-GO thread gauges the first time:
- Full thread designation with tolerance class, e.g. M10x1.25-6H or 3/8-24 UNF-2B
- Plug, ring or both, and whether you need GO only, NO-GO only or complete sets
- Whether the gauges are for pre-plate or post-plate inspection
- Quantity, and whether a set is intended as a referee gauge
- Certificate requirement (ISO/IEC 17025 calibration certificate available on request)
- Your customer’s drawing or gauge specification if you need to match it
Need Referee or Replacement Thread Gauges?
Send the thread callout, class, gauge types and quantity. We review the specification and reply with price and lead time within 24 hours.
Related: GO/NO-GO thread gauges · Reading calibration certificates · Thread plug gauge wear limits
Frequently Asked Questions
✓ 20+ years gauge manufacturing
✓ ISO 9001:2015 certified
✓ In-house CNC grinding & inspection
✓ Drawing / RFQ reply within 24h
Order GO/NO-GO Thread Gauges for Supplier–Customer Alignment
GageTools manufactures GO/NO-GO thread plug and ring gauges for metric, unified, pipe and special threads, supplied as working sets or referee sets. ISO/IEC 17025 calibration certificate available on request. Standard sizes ship from stock within 72 hours; custom gauges in 10–15 working days. MOQ 1 piece. WhatsApp for fastest response.
💬 WhatsApp Quote 📐 Send Drawing for Quote