Need gauges for this? GageTools manufactures GO/NO-GO thread plug gauges and thread ring gauges in Dongguan, China. Standard sizes ship from stock within 72 hours, MOQ is 1 piece, and every RFQ gets a reply within 24 hours — request a quote.
What the Acme Thread Profile Looks Like
Acme threads were developed as a stronger, easier-to-make alternative to the square thread for moving loads. The profile is a trapezoid: two straight flanks at a 29° included angle, joined by a flat crest at the top and a flat root at the bottom.
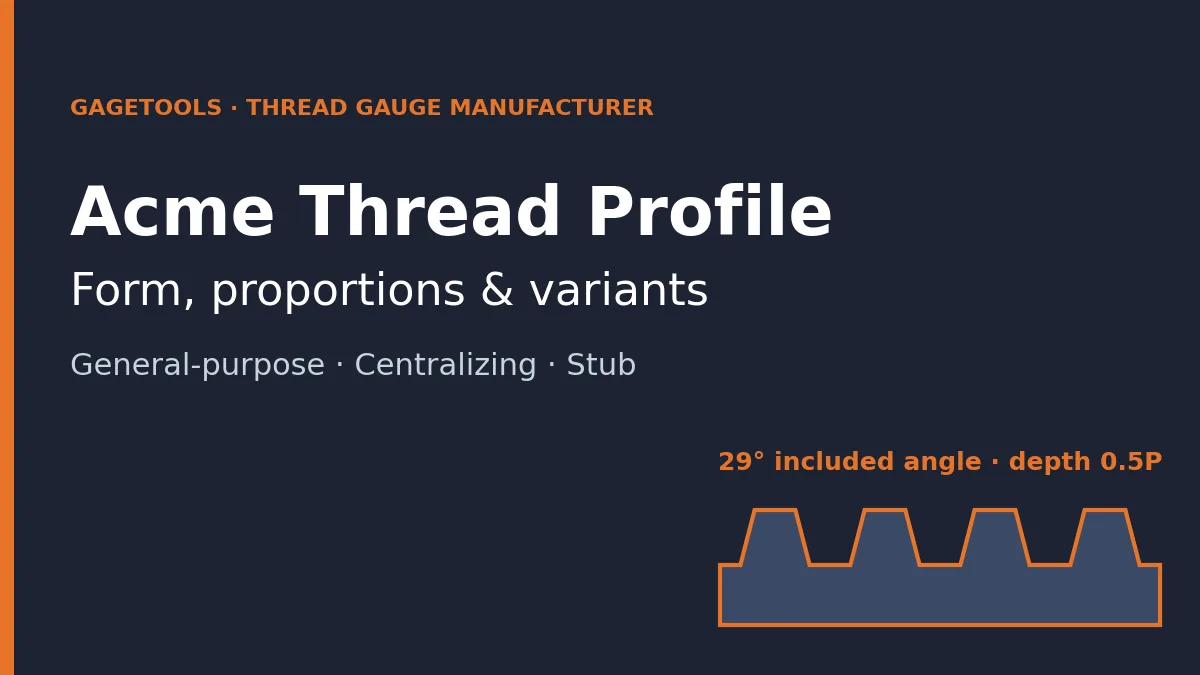
This page covers the profile itself — the geometry and its variants. For thread sizes, tolerances and the gauges used to inspect Acme threads, see our Acme thread gauge guide: sizes, tolerances and inspection.
Need GO/NO-GO gauges for this thread?
GageTools manufactures GO/NO-GO thread plug gauges from USD 20 and thread ring gauges from USD 30. MOQ 1 piece, stock sizes ship within 72 hours, and a calibration report or ISO 17025 certificate is available on request.
Thread Plug GaugesThread Ring GaugesRequest a QuoteBasic Profile Proportions
The basic profile is the theoretical form from which all tolerances and allowances are applied. The widely documented basic proportions for general-purpose Acme threads (ASME B1.5) are:
| Element | Basic value | Notes |
|---|---|---|
| Included angle | 29° | 14.5° each side of a line perpendicular to the thread axis |
| Basic thread height | 0.5P | General-purpose Acme; P = pitch |
| Basic flat at crest | 0.3707P | Flat width at the crest of the basic profile |
| Basic flat at root | 0.3707P | Flat width at the root of the basic profile |
| Pitch expression | Threads per inch (TPI) | e.g. 1-5 ACME-2G = 1″ major dia, 5 TPI |
These are basic values. Real threads include allowances and tolerances, and major, minor and pitch diameter limits depend on the size and class. For design and manufacturing, always use the full tables in the current edition of the standard rather than calculating from these ratios alone.
Basic is not actual. Clearance between internal and external Acme threads comes from allowances and class tolerances, not from the basic profile. A gauge made to the basic profile alone would not match any real class.
Why the Acme Profile Is Shaped This Way
Each feature of the Acme form has a practical reason:
- 29° flank angle: close enough to square to transmit load efficiently along the axis, but angled enough to be cut with a single-point tool, taps and dies, and to allow some take-up of wear with split nuts
- Flat crest and root: wide, strong thread roots resist shear and are less sensitive to damage than sharp V-threads
- Deep thread (0.5P): a generous flank contact area for load-bearing lead screws
- Coarse pitches: fast travel per turn for jacks, vises and actuators
The result is a thread that carries heavy axial load with reasonable efficiency, which is why Acme threads appear on machine-tool lead screws, lifting jacks, clamps and valve stems.
How to Read an Acme Thread Callout
An Acme callout tells you the size, the pitch, the profile variant and the class — everything needed to identify the correct thread profile and gauges. A typical example is 1-5 ACME-2G.
| Callout part | Example | Meaning |
|---|---|---|
| Nominal major diameter | 1 | 1 inch nominal size |
| Threads per inch | 5 | Pitch P = 1/5 inch = 0.2 inch |
| Thread form | ACME / STUB ACME | Full-depth or Stub Acme profile |
| Class | 2G, 3G, 4G or 2C–6C | General-purpose (G) or centralizing (C) fit |
| Hand | LH if shown | Left-hand; right-hand if not stated |
| Multi-start | e.g. 2 starts, lead stated | Lead = starts × pitch |
With the pitch known, the basic proportions follow directly. For 1-5 ACME-2G, P = 0.2 inch, so the basic thread height is 0.1 inch and the basic crest and root flats are about 0.074 inch. The class then decides how far the actual thread sits below or above those basic dimensions.
General-Purpose vs Centralizing vs Stub Acme
All Acme threads share the 29° angle, but they differ in thread height and in how the mating threads are allowed to fit.
- Basic thread height 0.5P
- Clearance on major and minor diameters
- Flanks carry the load
- Most common type for lead screws and jacks
General-purpose threads are not designed to centralize: under radial load the screw can shift sideways and bear on the major or minor diameter.
- Same 29° form
- Controlled, closer fit on the major diameter
- Keeps the screw centred in the nut
- Used where wedging must be avoided
Centralizing classes limit radial movement so the flanks cannot wedge under side load. They need tighter control of the major diameter.
| Variant | Standard | Basic height | Typical use |
|---|---|---|---|
| General-purpose Acme | ASME B1.5 | 0.5P | Lead screws, jacks, vises, clamps |
| Centralizing Acme | ASME B1.5 | 0.5P | Screws under side load, precision drives |
| Stub Acme | ASME B1.8 | 0.3P | Thin walls, limited depth, heat-treated parts |
Stub Acme keeps the 29° angle but reduces the basic height to 0.3P. It is used where a full-depth Acme thread would weaken a thin-walled part or where the thread must be shallow.
Acme vs Trapezoidal, Square and Buttress Profiles
Acme is one of several power-transmission thread forms. The most common confusion is between Acme and metric trapezoidal threads, which look almost identical.
| Thread form | Flank angle | Standards | Key difference |
|---|---|---|---|
| Acme | 29° included | ASME B1.5, B1.8 (Stub) | Inch, TPI-based pitches |
| Trapezoidal (Tr) | 30° included | ISO 2901–2904, DIN 103 | Metric, pitch in mm |
| Square | 0° (flanks perpendicular) | No single common standard | Highest efficiency, harder to make |
| Buttress | 7° load flank / 45° trailing flank | ASME B1.9 | Load in one direction only |
Acme and Tr threads are not interchangeable. The 1° angle difference and the inch vs metric pitch mean an Acme nut will not run correctly on a trapezoidal screw even when the diameters look similar. Metric trapezoidal threads are covered in our trapezoidal thread gauge guide.
How the Acme Profile Affects Gauging
The profile determines what a thread gauge must check. Acme gauging follows the same GO/NO-GO logic as other threads, with some profile-specific points:
- GO gauges carry the full 29° form with correct lead, so they check functional size — the combined effect of pitch diameter, lead and flank angle
- NO-GO gauges check pitch diameter only, with a shortened thread length
- Class matters: 2G, 3G, 4G and centralizing classes each need their own gauge limits; a 2G gauge cannot be used for 3G parts
- Stub Acme needs Stub Acme gauges: the 0.3P height means full-depth Acme gauges will not fit
- Multi-start Acme: gauges must match the lead as well as the pitch
Because Acme threads are coarse and deep, a small flank-angle error has a large effect on fit. That is why functional GO gauges are so important on lead screws and nuts. Standard thread plug gauges and ring gauges for Acme sizes are available, and special Acme forms can be made from drawings.
Common Acme Profile Mistakes
| Mistake | Consequence | How to avoid |
|---|---|---|
| Treating Acme and Tr as the same | Nut and screw do not run; wrong gauges bought | Check the callout: ACME (inch, 29°) vs Tr (metric, 30°) |
| Ignoring the class (G vs C) | Wedging under side load, or wrong gauges | Read the full callout including class letter |
| Using full-depth gauges on Stub Acme | Gauges will not enter or run on | Order Stub Acme gauges to ASME B1.8 |
| Calculating limits from basic ratios only | Gauges and parts without clearance | Use the standard’s tables for each size and class |
| Forgetting multi-start lead | GO gauge will not engage | State number of starts and lead in the RFQ |
What to Send When Ordering Acme Thread Gauges
To quote Acme thread gauges accurately, send:
- Full callout, e.g.
1-5 ACME-2G,3/4-6 ACME-3Cor1/2-10 STUB ACME-2G - Right-hand or left-hand, and number of starts
- Plug gauges (for nuts), ring gauges (for screws) or both, GO and NO-GO
- Quantity, and any customer gauge specification
- Certificate requirement (ISO/IEC 17025 available on request)
For non-standard Acme forms, send the drawing to our custom thread gauge team and we will confirm the gauge design before quoting.
Need Acme Thread Gauges?
Send the Acme callout, class, hand, number of starts and quantity. We reply with price and lead time within 24 hours. Custom forms in 10–15 working days.
Related: Acme thread gauge guide · Trapezoidal thread gauges · Custom thread gauges
Frequently Asked Questions
✓ 20+ years gauge manufacturing
✓ ISO 9001:2015 certified
✓ In-house CNC grinding & inspection
✓ Drawing / RFQ reply within 24h
Order Acme and Stub Acme Thread Gauges
GageTools manufactures GO/NO-GO Acme, Stub Acme and trapezoidal thread plug and ring gauges, plus custom power-thread gauges from your drawing. ISO/IEC 17025 calibration certificate available on request. Standard sizes ship from stock within 72 hours; custom gauges in 10–15 working days. MOQ 1 piece. WhatsApp for fastest response.
💬 WhatsApp Quote 📐 Send Drawing for Quote