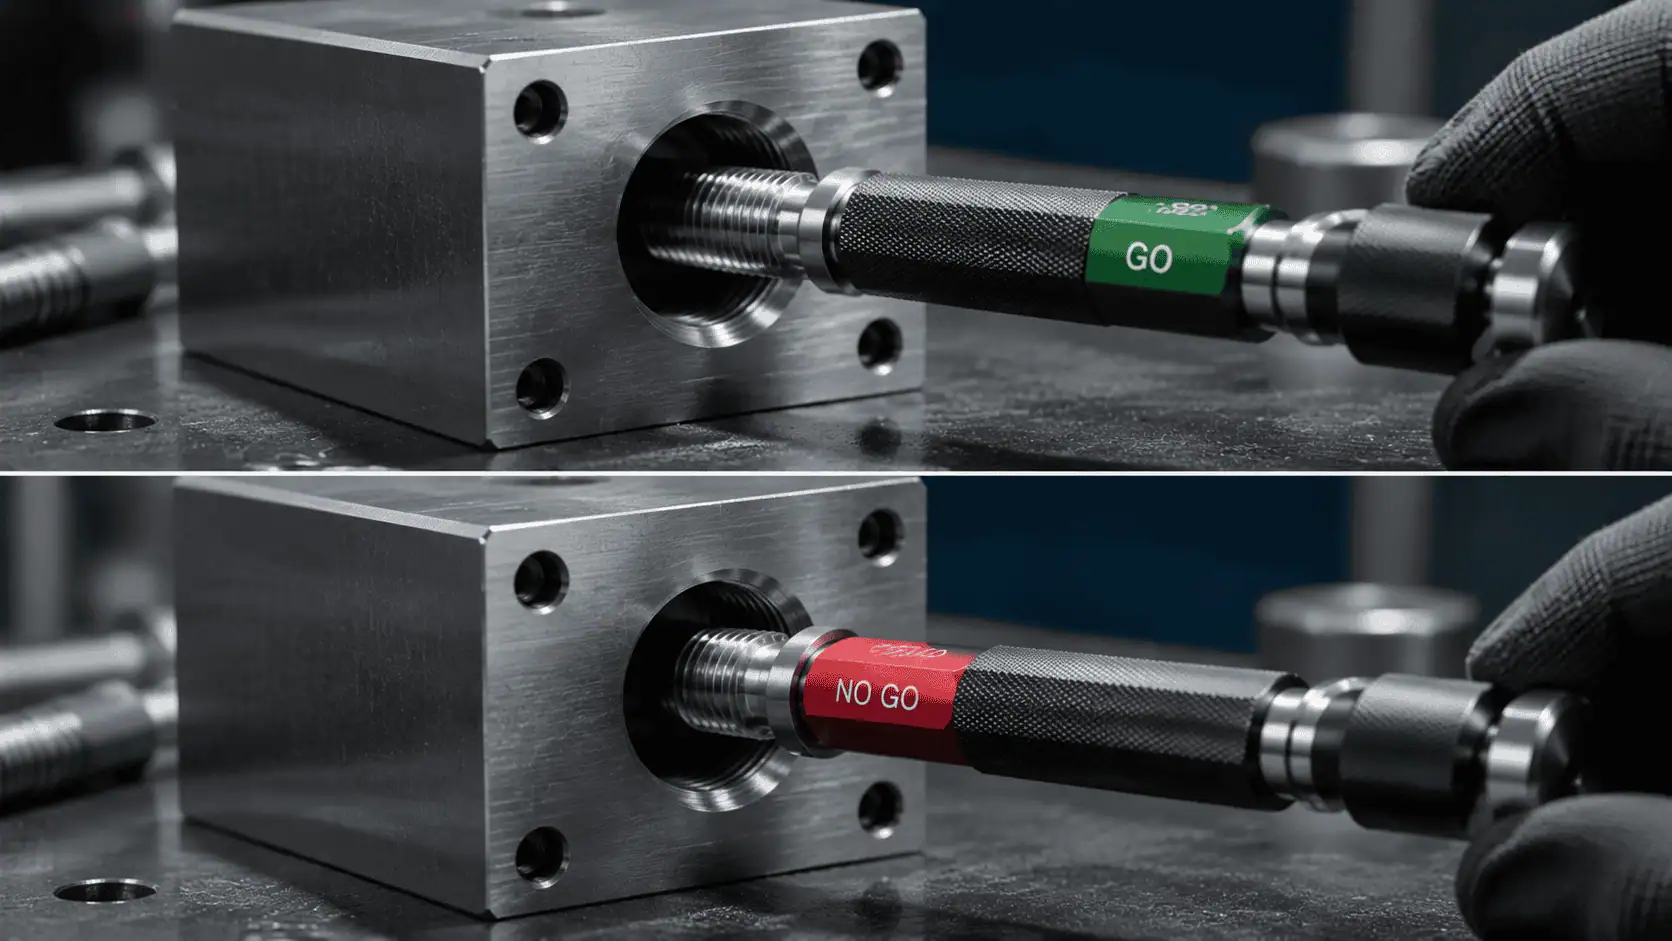
Need gauges for this? GageTools manufactures GO/NO-GO thread plug gauges and thread ring gauges in Dongguan, China. Standard sizes ship from stock within 72 hours, MOQ is 1 piece, and every RFQ gets a reply within 24 hours — request a quote.
Why the Callout Decides Which Gauge Is Ordered
Thread gauges are made to one designation and one class. A GO/NO-GO plug for M10x1.5-6H cannot inspect M10x1.25-6H, and a 2B plug is the wrong gauge for a 3B thread. When a drawing says only “M10” or “1/4 UNC”, purchasing has to guess, and a wrong guess means either wrong gauges or parts accepted to the wrong limits.
A complete callout lets the buyer, the machinist, the inspector and the gauge maker all read the same requirement. It also prevents the most common reason for returned gauges: a gauge made exactly to an incomplete order.
Think of the callout as a purchase specification for three things at once: the cutting tool, the inspection method and the gauge. If a tap can be selected from the callout but a gauge cannot, the callout is incomplete. The sections below list what each thread system needs.
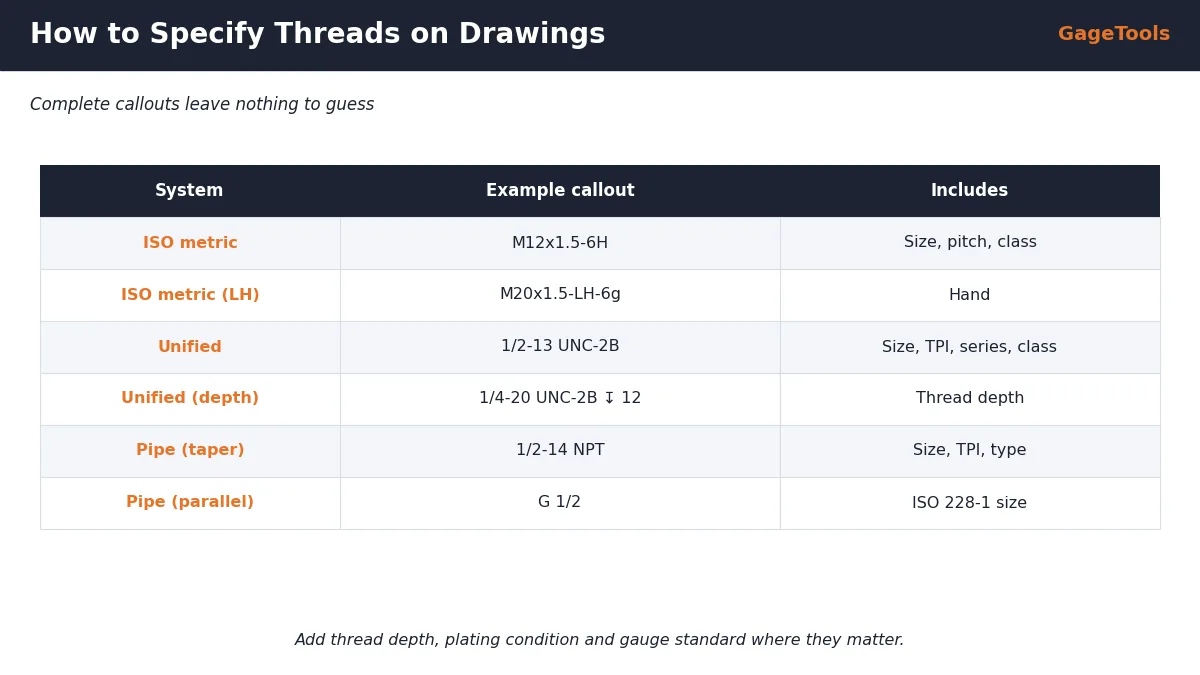
Metric Thread Callouts (ISO 965 / ISO 68-1)
ISO metric threads are designated by the letter M, nominal diameter, pitch and tolerance class. The pitch of coarse threads is often omitted, but writing it out removes any doubt.
| Callout | Meaning | Gauge needed |
|---|---|---|
| M10x1.5-6H | Coarse internal thread, class 6H | GO/NO-GO plug, 6H |
| M10x1.25-6g | Fine external thread, class 6g | GO/NO-GO ring, 6g |
| M8x1-5g6g | Separate pitch and crest diameter classes | Ring to 5g pitch diameter; crest per 6g |
| M12x1.5-LH-6H | Left-hand internal thread | Left-hand GO/NO-GO plug, 6H |
| M6-6H | Coarse pitch implied (1 mm) | GO/NO-GO plug M6x1-6H |
For internal threads with tolerance position H, the GO plug is the same for 4H, 5H, 6H and 7H, because the fundamental deviation is zero; only the NO-GO plug differs. For position G the GO plug is different. So the class on the drawing matters most for the NO-GO gauge, and a missing class is not a small detail. More in our guide to thread tolerance classes 4H to 6e.
Unified Inch Thread Callouts (ASME B1.1)
Unified threads are designated by nominal size, threads per inch, series and class, with A for external and B for internal threads.
| Callout | Meaning | Gauge needed |
|---|---|---|
| 1/4-20 UNC-2A | Coarse series, external, class 2A | GO/NOT GO ring, 2A |
| 1/4-28 UNF-3B | Fine series, internal, class 3B | GO/NOT GO plug, 3B |
| #10-32 UNF-2B | Numbered size, internal, class 2B | GO/NOT GO plug, 2B |
| 1/2-13 UNC-2B-LH | Left-hand internal thread | Left-hand plug, 2B |
| 3/8-24 UNF-2A (21) | Gauging system 21 per ASME B1.3 | GO/NOT GO ring, 2A |
Class 2A/2B is the general-purpose fit; 3A/3B is tighter. The choice changes both GO and NOT GO gauges for external threads, because class 2A has an allowance and 3A does not. See thread class 2B vs 3B gauge selection.
Pipe Thread Callouts: NPT, NPTF, BSPP and BSPT
Pipe threads are the area where incomplete callouts cause the most trouble, because similar-looking designations need completely different gauges.
Never write just “1/2 BSP” or “1/2 pipe”. G (ISO 228) and Rp (ISO 7) are both parallel internal threads but belong to different standards with different purposes; R and Rc are taper. For external G threads, ISO 228 has two tolerance classes, A and B, which should appear in the callout. Our NPT vs NPTF vs BSPP vs BSPT guide explains the gauges for each.
NPT and NPTF are not interchangeable on a drawing. NPTF dryseal threads need additional gauging beyond the L1 check. If the part must seal without sealant, the callout must say NPTF, or the wrong gauges will be ordered.
Thread Length, Depth and Blind Holes
The designation says what the thread is; the length or depth says how much of it must be good. Gauging depends on both.
- Blind holes: give the minimum full-thread depth and the drill depth separately, e.g. “M8x1.25-6H, full thread 16 min, drill 20”. The GO plug must reach the full-thread depth.
- Through holes: state that the thread is through, so the inspector knows the GO plug must pass the whole length.
- External threads: give the minimum full-thread length, and whether a runout or undercut is allowed.
- Deep threads: if the full-thread depth exceeds the length of a standard GO plug, the gauge must be made longer; say so in the RFQ.
Our guide to thread gauges for blind holes covers depth marking and clearance.
Left-Hand, Multi-Start and Special Threads
Anything that is not a single-start right-hand thread must be stated explicitly. A gauge maker will assume right-hand single-start if the callout is silent.
- Left-hand: add LH to the designation, for example M12x1.5-LH-6H or 1/2-13 UNC-2B-LH. Left-hand gauges are made to order; see left-hand thread gauges.
- Multi-start: give lead and pitch, and the number of starts.
- Trapezoidal and Acme: give size, pitch or TPI and class, for example Tr20x4-7H or 1/2-10 ACME-2G.
- Buttress (ASME B1.9) and special forms: reference the standard or provide full profile dimensions.
Coating, Plating and the Gauging System
Two notes on the drawing prevent most gauge disputes: when the thread dimensions apply, and how the thread is to be gauged.
| Drawing note | Why it matters for gauging |
|---|---|
| Dimensions apply after coating | Final acceptance gauges are for the finished size; the machine shop must leave room for the coating |
| Dimensions apply before coating | Gauges are used before plating; coated parts are not checked with the same gauges |
| Gauging per ISO 1502 | Standard GO/NO-GO gauging for metric threads, NO-GO not more than 2 turns |
| Gaging system 21 per ASME B1.3 | GO/NOT GO attribute gauging for unified threads |
| Gaging system 22 or 23 per ASME B1.3 | Additional element measurement required — gauges alone are not enough |
ASME B1.3 defines gauging systems 21, 22 and 23 for unified inch threads. System 21 relies on GO and NOT GO gauges; systems 22 and 23 add measurement of further thread elements. If the drawing specifies a system beyond 21, make sure receiving inspection has the equipment to meet it. For plating, see thread gauges before or after plating.
Common Callout Mistakes and Their Consequences
Each of these gaps can be closed by the design engineer in a few minutes. Left open, they cost days of clarification between purchasing and the gauge maker, or result in gauges that do not match the real requirement.
A simple check helps: before a drawing is released, ask whether an inspector who has never seen the part could pick the correct GO and NO-GO gauges from the callout alone. If not, the callout needs more detail.
What to Send When Ordering Gauges From a Drawing
We make standard thread plug gauges and ring gauges from stock, and special gauges from your drawing. To quote correctly, send:
- The part drawing, or the full thread callouts copied from it
- Tolerance class for every thread, and LH where applicable
- Full-thread depth or length, especially for deep blind holes
- Whether gauging is before or after coating
- Gauging standard or system required by your customer
- Quantity, plug or ring, and certificate requirement (ISO/IEC 17025 available on request)
If anything is missing or unclear, we will ask before quoting, and we confirm the gauge design with you before manufacture.
Have a Drawing With Thread Callouts?
Send the drawing or the thread list. We check each callout, confirm the gauge design and reply with price and lead time within 24 hours.
Related: Custom thread gauges from drawing · How to order custom thread gauges · Thread charts
Frequently Asked Questions
✓ 20+ years gauge manufacturing
✓ ISO 9001:2015 certified
✓ In-house CNC grinding & inspection
✓ Drawing / RFQ reply within 24h
Order Thread Gauges That Match Your Drawing
GageTools manufactures GO/NO-GO thread plug and ring gauges for metric, unified, pipe, Acme, trapezoidal and special threads, made to your drawing. ISO/IEC 17025 calibration certificate available on request. Standard sizes ship from stock within 72 hours; custom gauges in 10–15 working days. MOQ 1 piece. WhatsApp for fastest response.
💬 WhatsApp Quote 📐 Send Drawing for Quote